
PLC controlled vertical hardening scanners
A scanning hardening machine: the part traverses through the coil while quench follows behind it.
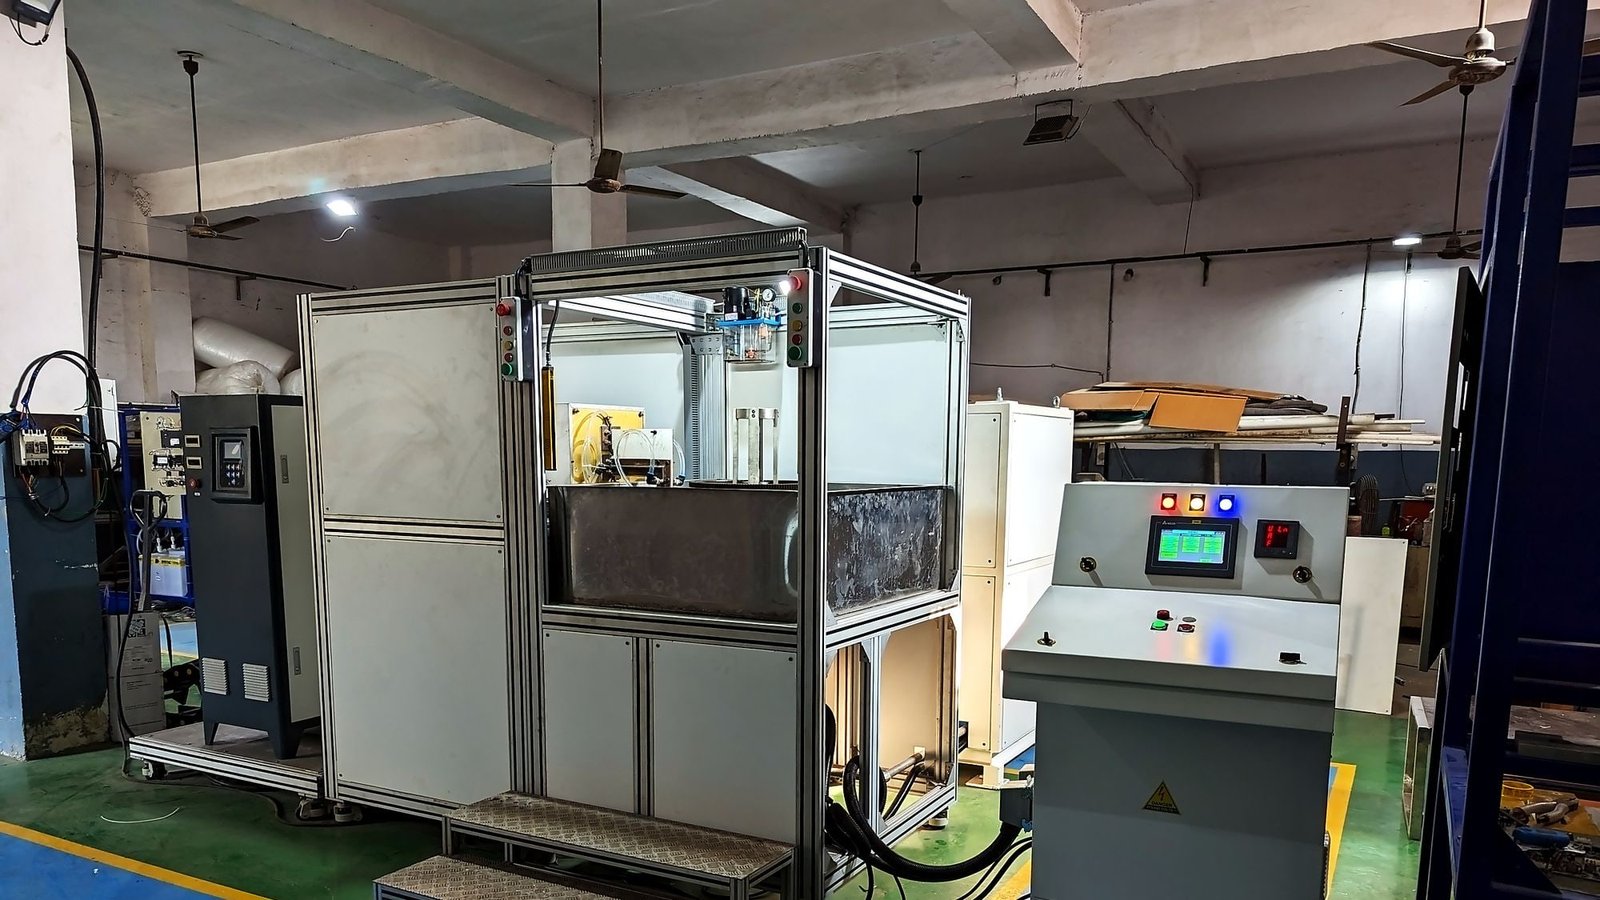
In a scanning machine the coil and the quench ring stay put and the part travels through them, or the head travels along the part. Only a short band is hot at any moment, and quench follows a fixed distance behind. That makes it possible to harden a shaft far longer than any coil could heat at once, at a repeatable case depth, using a fraction of the power a single-shot approach would need.
Our PLC controlled vertical scanner is built for auto components, tractor parts and JCB components, with standard programs suitable for a range of components, and an inbuilt DM water and quenching water cooling and circulation system.
We configure our vertical scanners for shafts from 20 mm to 120 mm diameter, case depths from 0.8 mm to 5 mm and travel from 10 mm to 1500 mm, with ABE-40 kW to ABE-120 kW power supplies. Your component and process determine the final specification.
A double station variant is built for higher throughput, and the same architecture underlies the sledge hammer head hardening machine, where two stations alternate so the operator is always loading one while the other runs.
Technical specifications
- Shaft diameter20 mm to 120 mm0.79 in to 4.72 in
- Case depth0.8 mm to 5 mm0.031 in to 0.197 in
- Travelling length10 mm to 1500 mm0.39 in to 59.1 in
- Power supplyABE-40 kW to ABE-120 kW
- ControlPLC, with standard programs for a range of components
- CoolingInbuilt DM water and quenching water cooling and circulation
- StationsSingle or double
We confirm the final configuration against your component, material and production requirements.
Questions engineers ask
Why scan instead of heating the whole part at once?
Single-shot hardening needs enough power to bring the entire hardened length to temperature simultaneously. On a 1200 mm shaft that is an enormous power supply and a very large coil. Scanning heats a short band and moves, so the same result comes from a far smaller machine, and the case depth stays consistent along the length.
What sets the case depth on a scanner?
Mainly frequency and scan speed. Higher frequency concentrates the current in a thinner skin; slower travel gives heat more time to conduct inward. The PLC holds both constant so part 1 and part 5000 come out the same.
What is DM water and why does the machine need it?
Demineralised water. The coil and the power electronics are water cooled, and ordinary water would deposit scale and conduct current where it should not. The machine carries its own DM water circuit, separate from the quench circuit.
Related processes
Industries served
- Automotive componentsShafts, gears, bushes, axle shafts and flywheel rings, at production rate.
- Tractor and agricultural equipmentParts that work in soil and abrasion, where wear resistance decides service life.
- Construction and earthmoving equipmentPins, bushes and linkage components that carry load and abrasion together.
- Hand toolsSledge hammers, claw hammers, chisels, pick axes and hoes, forged and hardened.
Tell us about the part.
Send a drawing, the material, the case depth or temperature you need, and your production rate. Our engineers will help define the right machine for your process.