
Induction power supply
ABE-50AB
50kW
Shaft and bush hardening up to 60 mm diameter. The most widely built model.
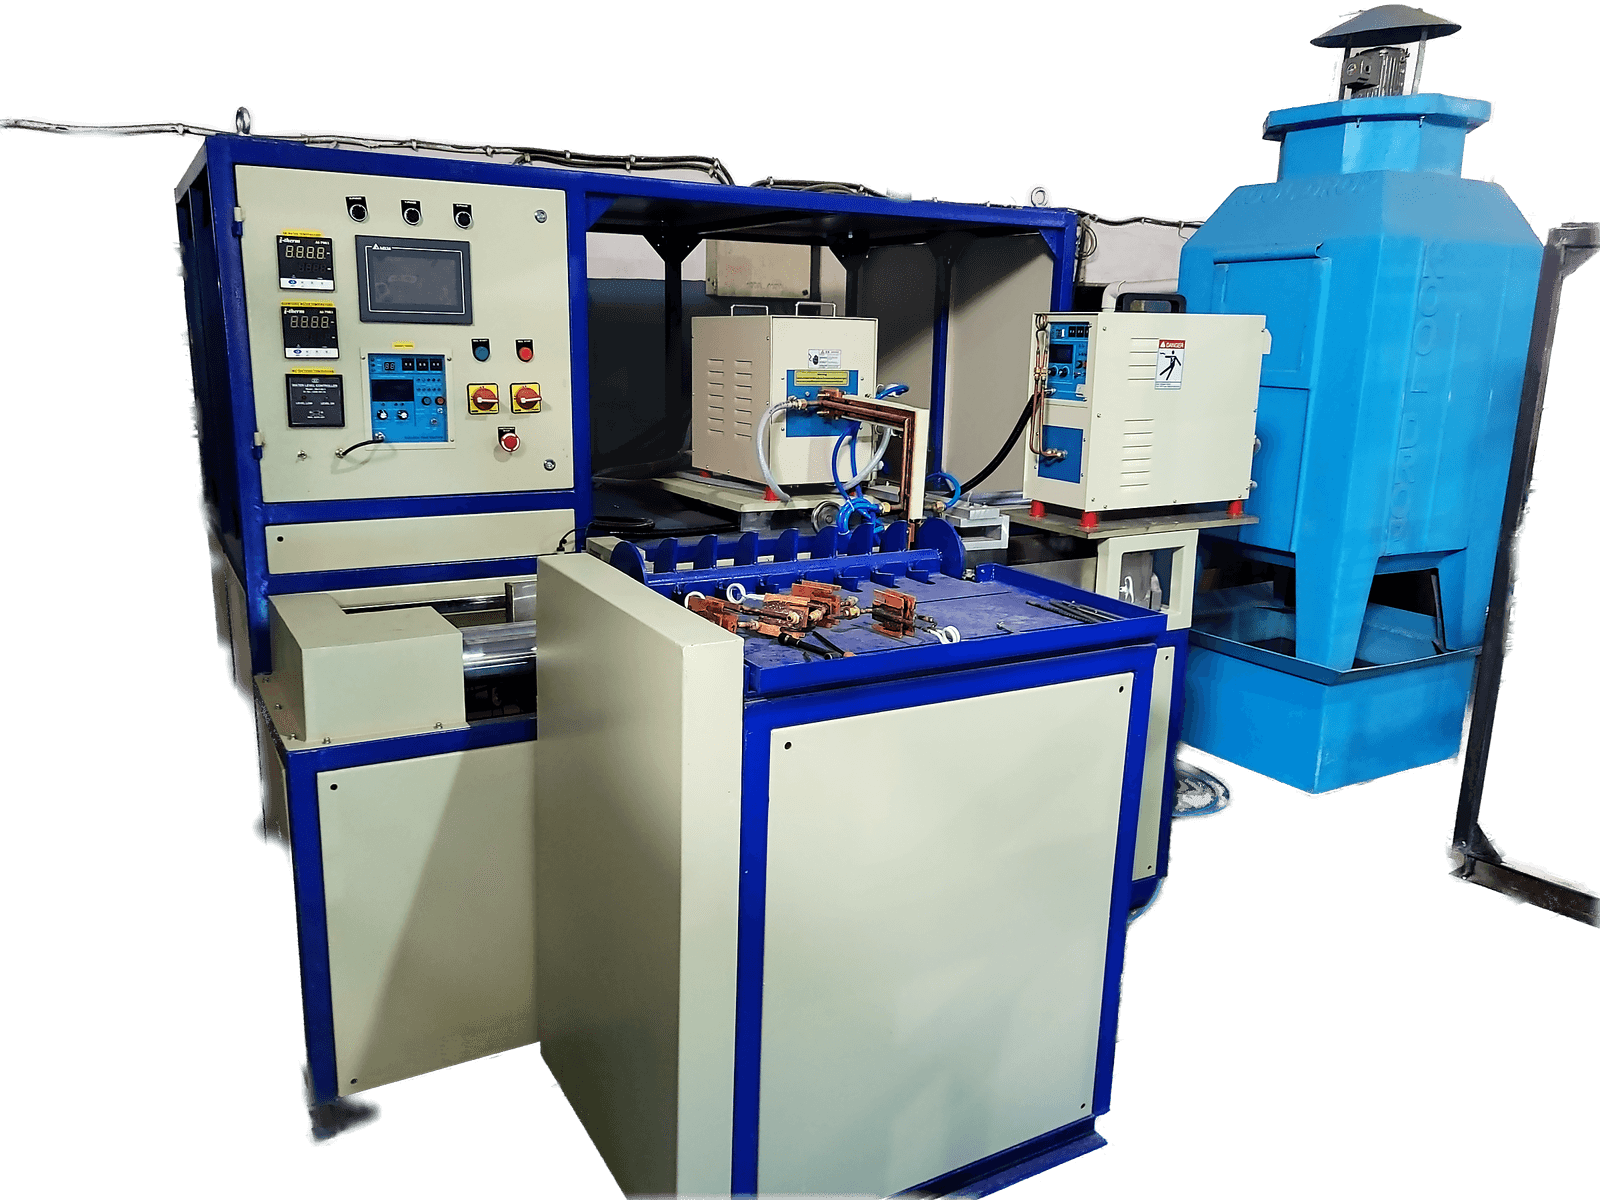
We have built the 50 kW ABE-50AB into horizontal and vertical hardening machines, axle shaft machines and CI ring and bush heating systems.
We use this 50 kW power class for shaft and bush hardening, with configurations for shaft diameters up to 60 mm. We also tailor machines for gears, bushes, JCB and tractor parts, axle shafts and flywheel rings.
The same 50 kW supply also drives high frequency work for induction hardening of auto components, tractor parts, hand tool hardening and agricultural tool hardening, and is supplied with a DM water chiller where continuous duty demands it.
Technical specifications
| Parameter | Specification |
|---|---|
| Output power | 50 kW. We confirm the duty cycle for your application. |
| Oscillation frequency | We select the frequency for your material, heating zone and required case depth. |
| Input power supply | We confirm the voltage, phase, frequency and connected load in your quotation. |
| Cooling water requirement | We specify the water flow, pressure, quality and cooling circuit for your machine configuration. |
| PLC / automation interface | Manual, PLC or CNC control options. We confirm communications and I/O with your automation requirements. |
| Compatible steels and alloys | We assess your material grade and heat treatment requirements before confirming suitability. |
| Maximum shaft diameter, hardening | 60 mm (2.36 in), subject to component and process review. |
| Switching technology | Solid-state IGBT |
Calculating required power? Run your cycle time on the Induction Power Estimator.
We select the frequency, dimensions, cooling and handling for your application. Send us your component drawing and required cycle time so we can confirm the complete machine specification.
Related processes
- Induction hardeningA hard, wear-resistant case on a tough core, in seconds, with the heat placed exactly where you want it.
- Induction brazingJoints that come out the same every time, because the heat is placed by a coil and timed by a machine.
- Induction annealingSoftening metal, relieving stress and restoring formability, on the section that needs it.
- Induction temperingTrading a little hardness for a lot of toughness, in line with the hardening machine.
- Induction shrink fittingAssembling interference fits by expanding the outer part instead of forcing it on.
- Induction pre-heatingBringing a component to a controlled temperature before the operation that follows.
- Induction bondingActivating an adhesive or bonding layer by heating the metal it is bonded to.
Related products
- Induction heating machinesIGBT power supplies from 5 kW to 500 kW, supplied standalone or built into a PLC or CNC controlled machine.
- Induction hardening machinesVertical and horizontal hardening machines for shafts, gears, bushes, axle shafts and flywheel rings.
- PLC controlled vertical hardening scannersA scanning hardening machine: the part traverses through the coil while quench follows behind it.
- Horizontal hardening machinesFor parts that must be supported along their length, or processed through stations in line.
- Induction brazing machinesRepeatable brazed joints with heat placed only where the filler must flow. Single and double station.
- Induction bonding machinesPLC controlled rotary machines for heat-activated bonding under controlled temperature and time.
- CI ring and bush heating machinesFully automatic PLC machines that pre-heat cast iron rings and bushes under closed-loop temperature control.
Tell us about the part.
Send a drawing, the material, the case depth or temperature you need, and your production rate. Our engineers will help define the right machine for your process.