
Gallery
Machines, inductors, and steel actually at temperature. All of it photographed at the Faridabad works, none of it stock imagery.
Machines
Our machines on our shop floor, ready for their next production line.
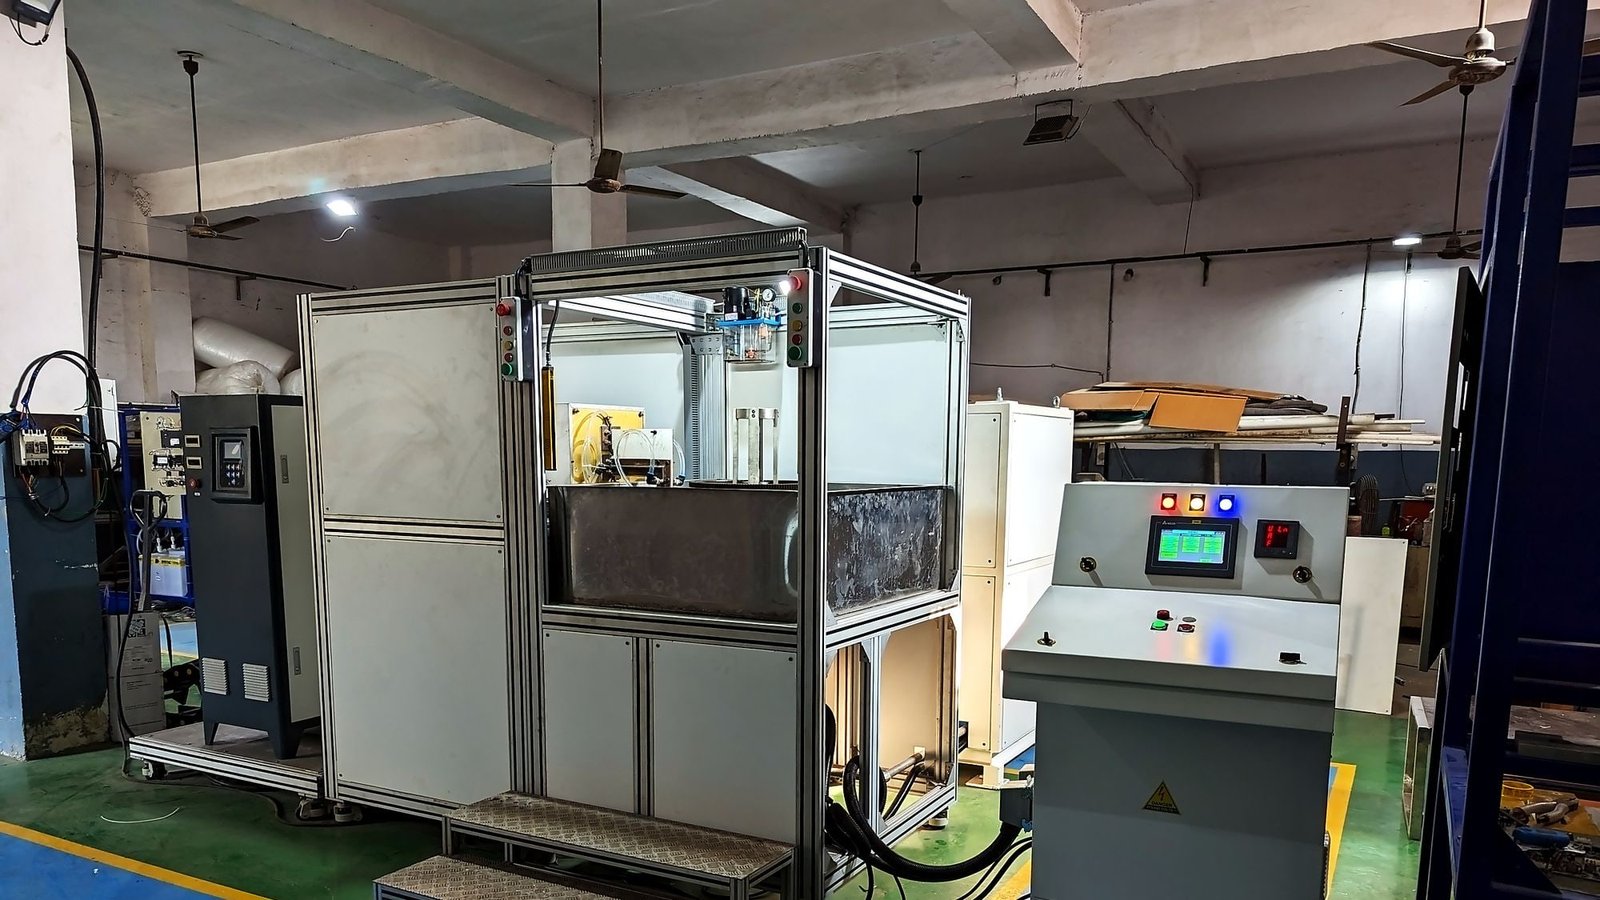
ABE-120AB flywheel ring hardening machine, 120 kW. 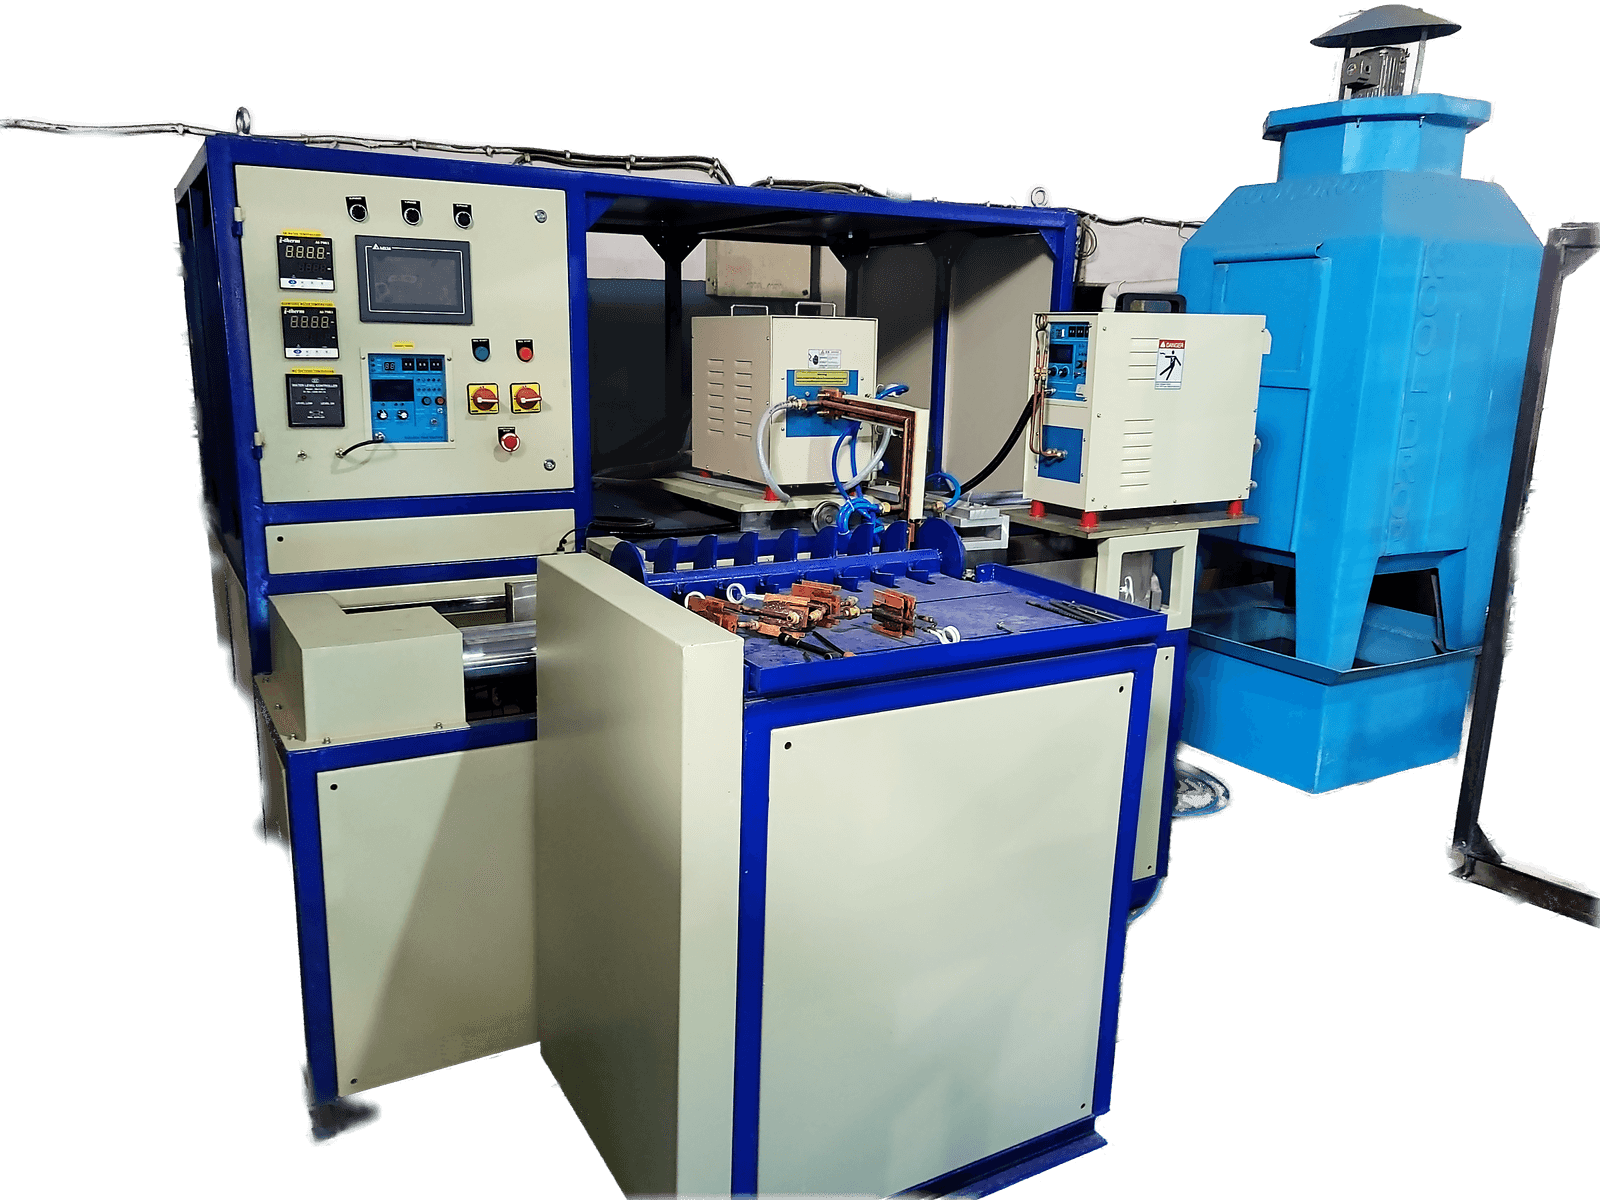
ABE-50AB horizontal hardening machine, with inductors laid out along the bed. 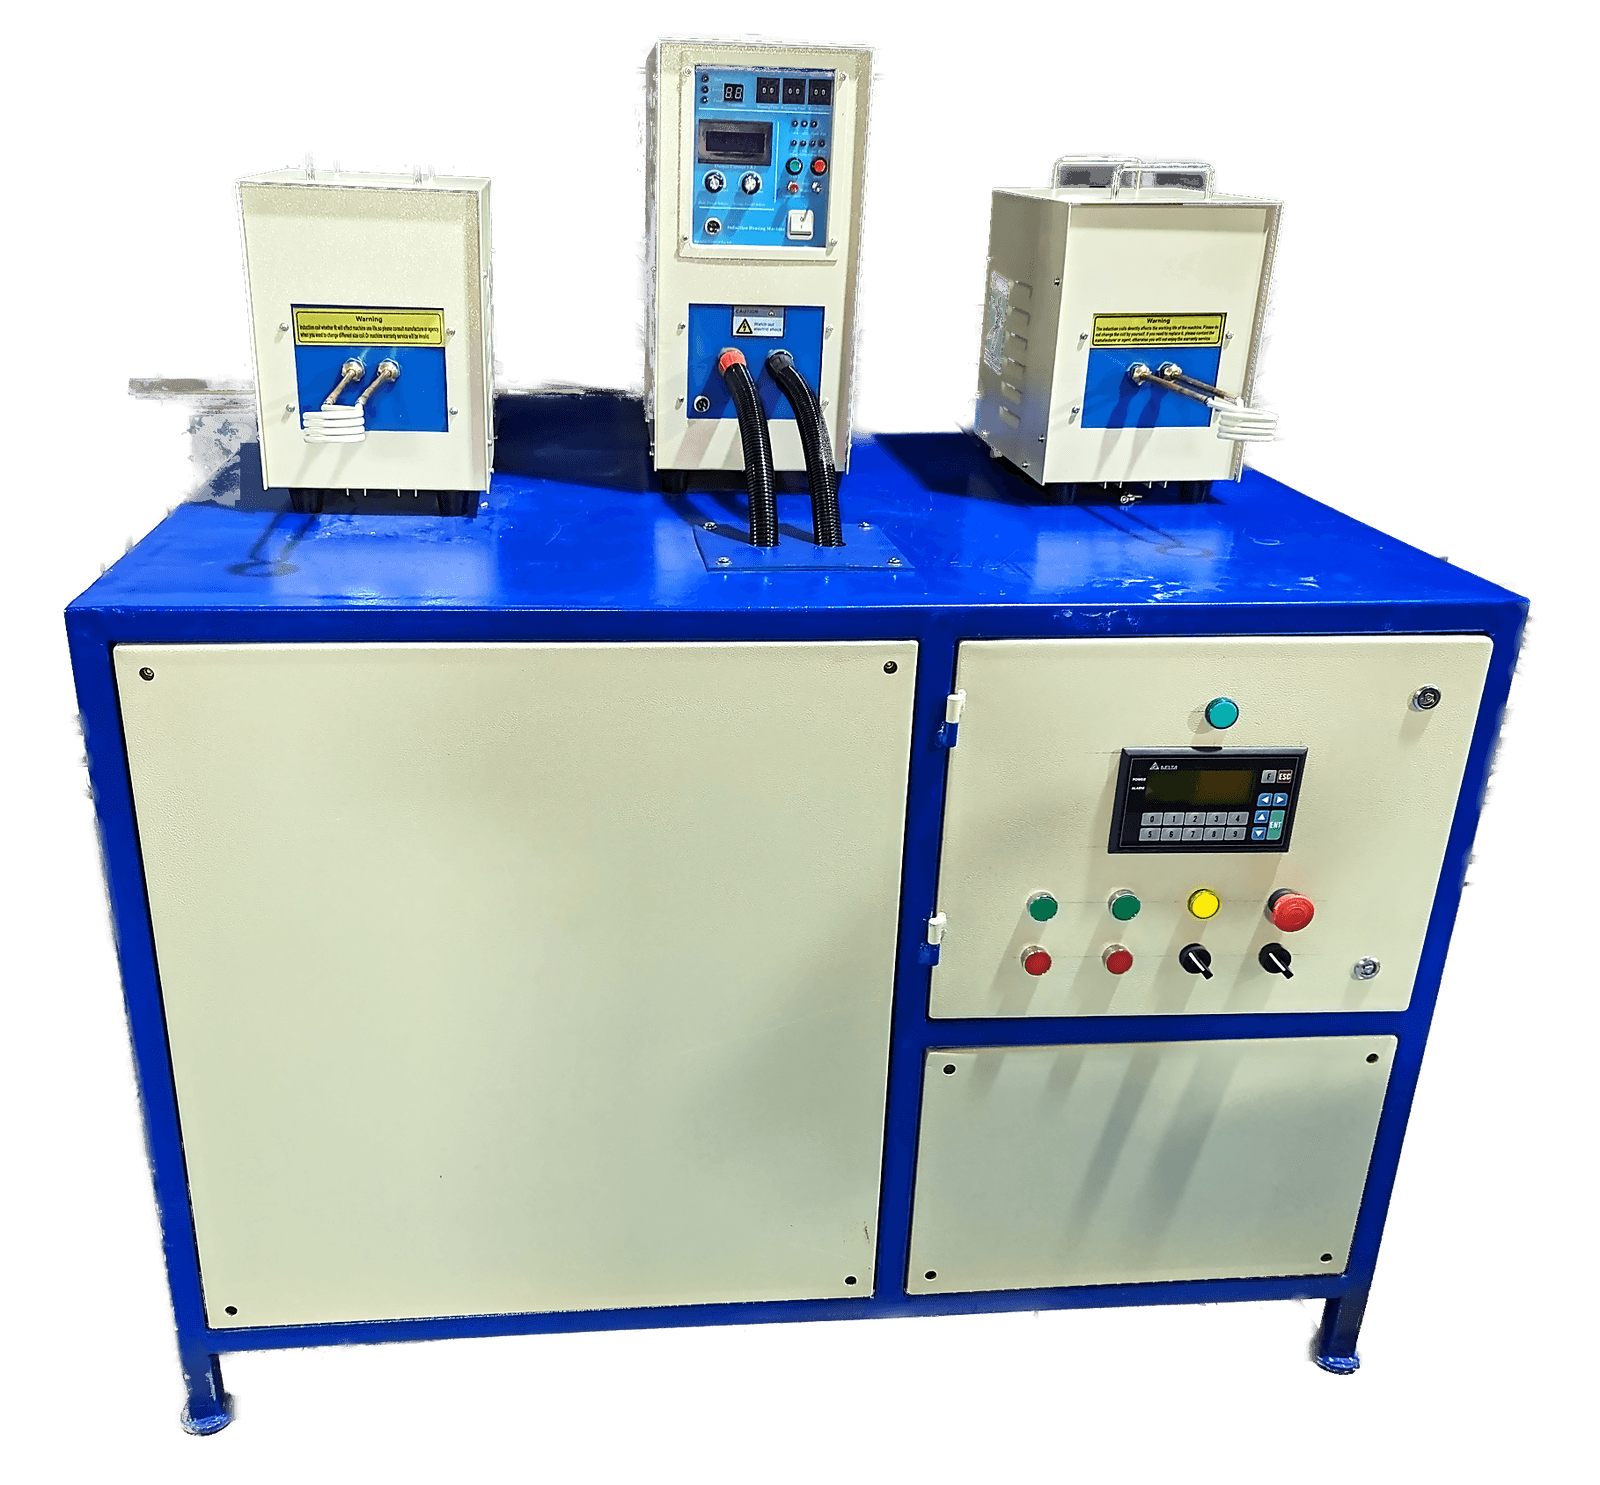
ABE-25AB double station induction brazing machine. 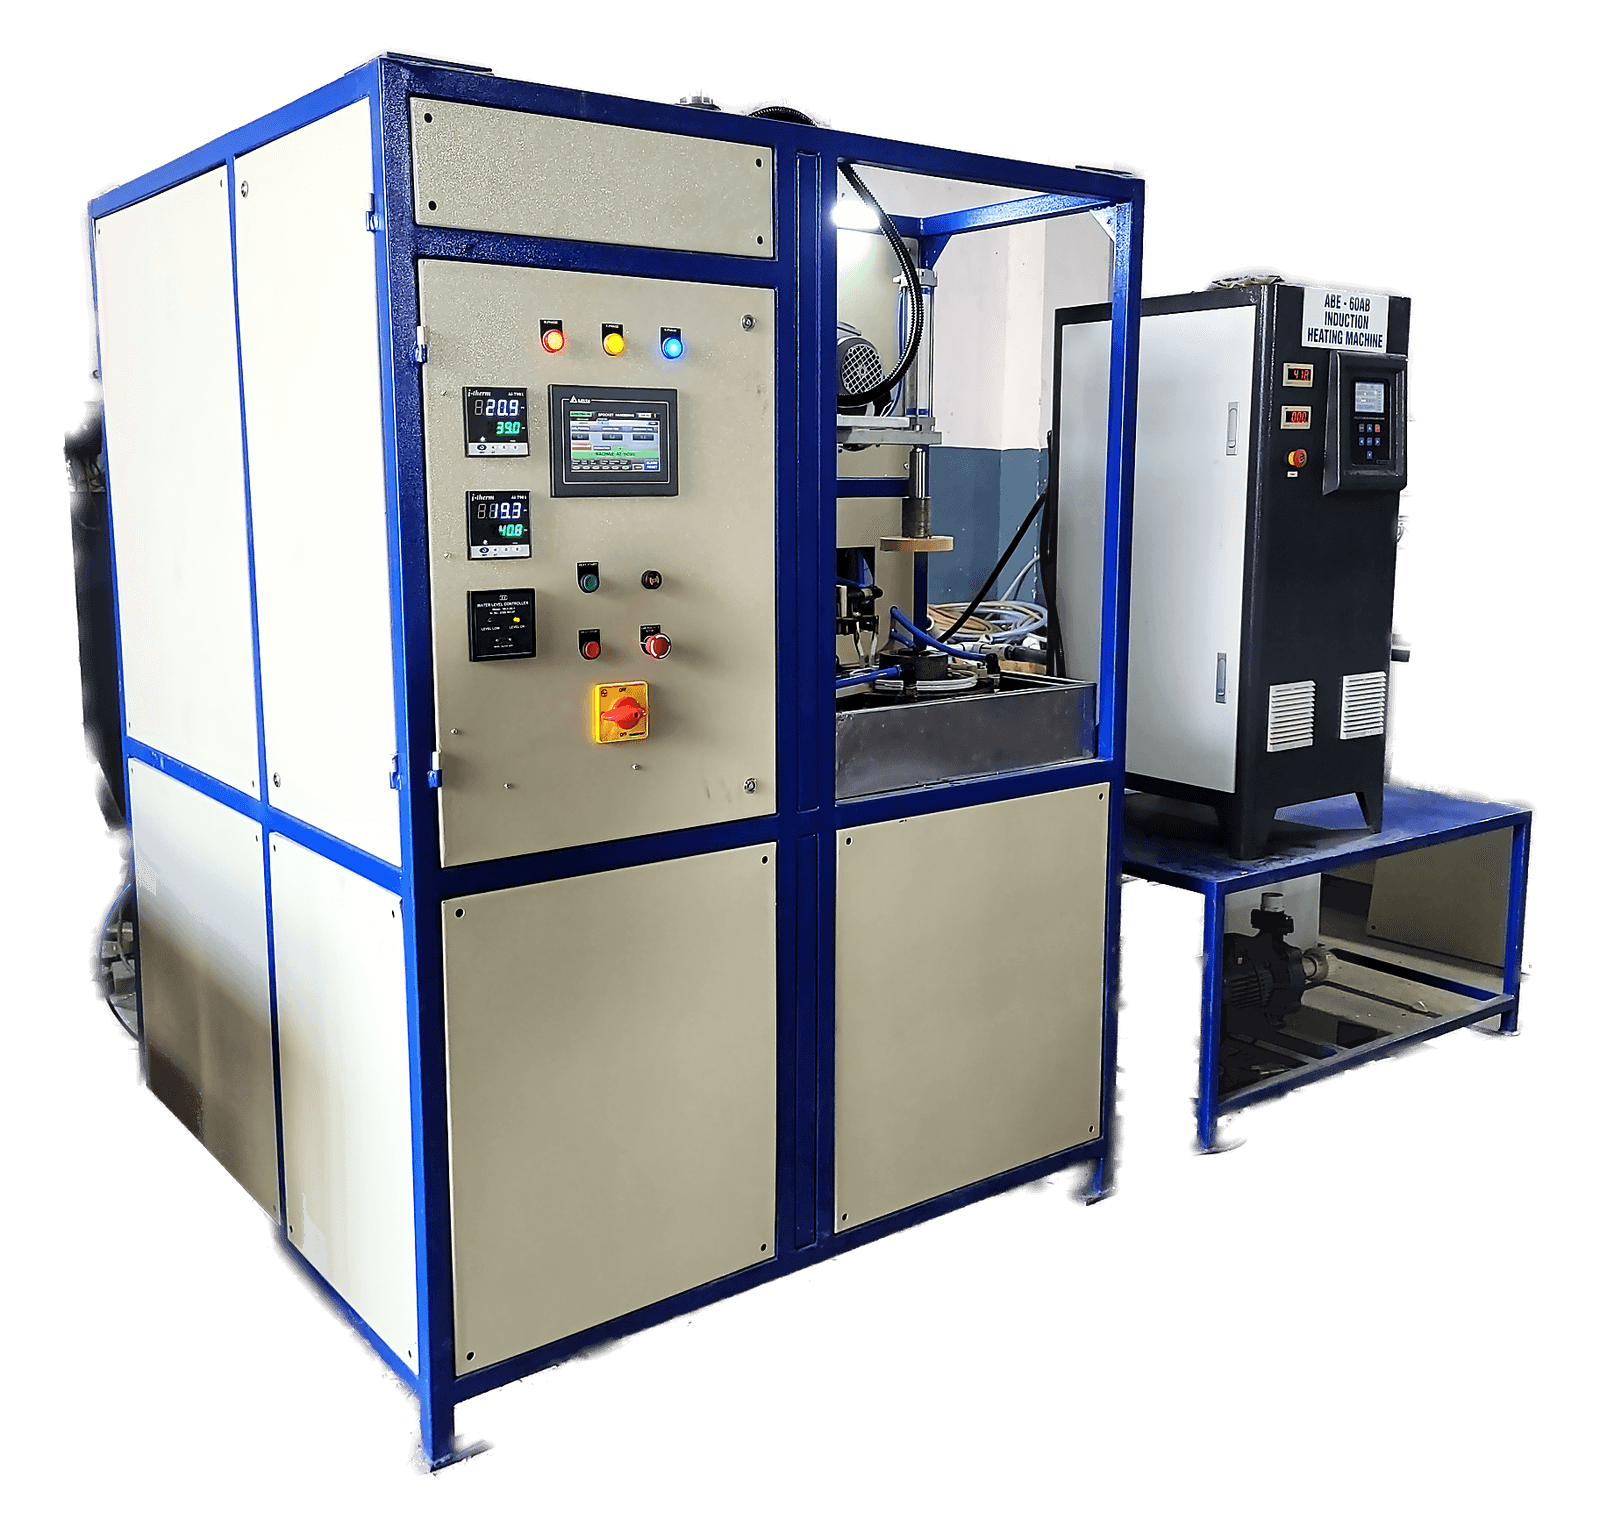
ABE-60AB induction hardening machine, 60 kW. 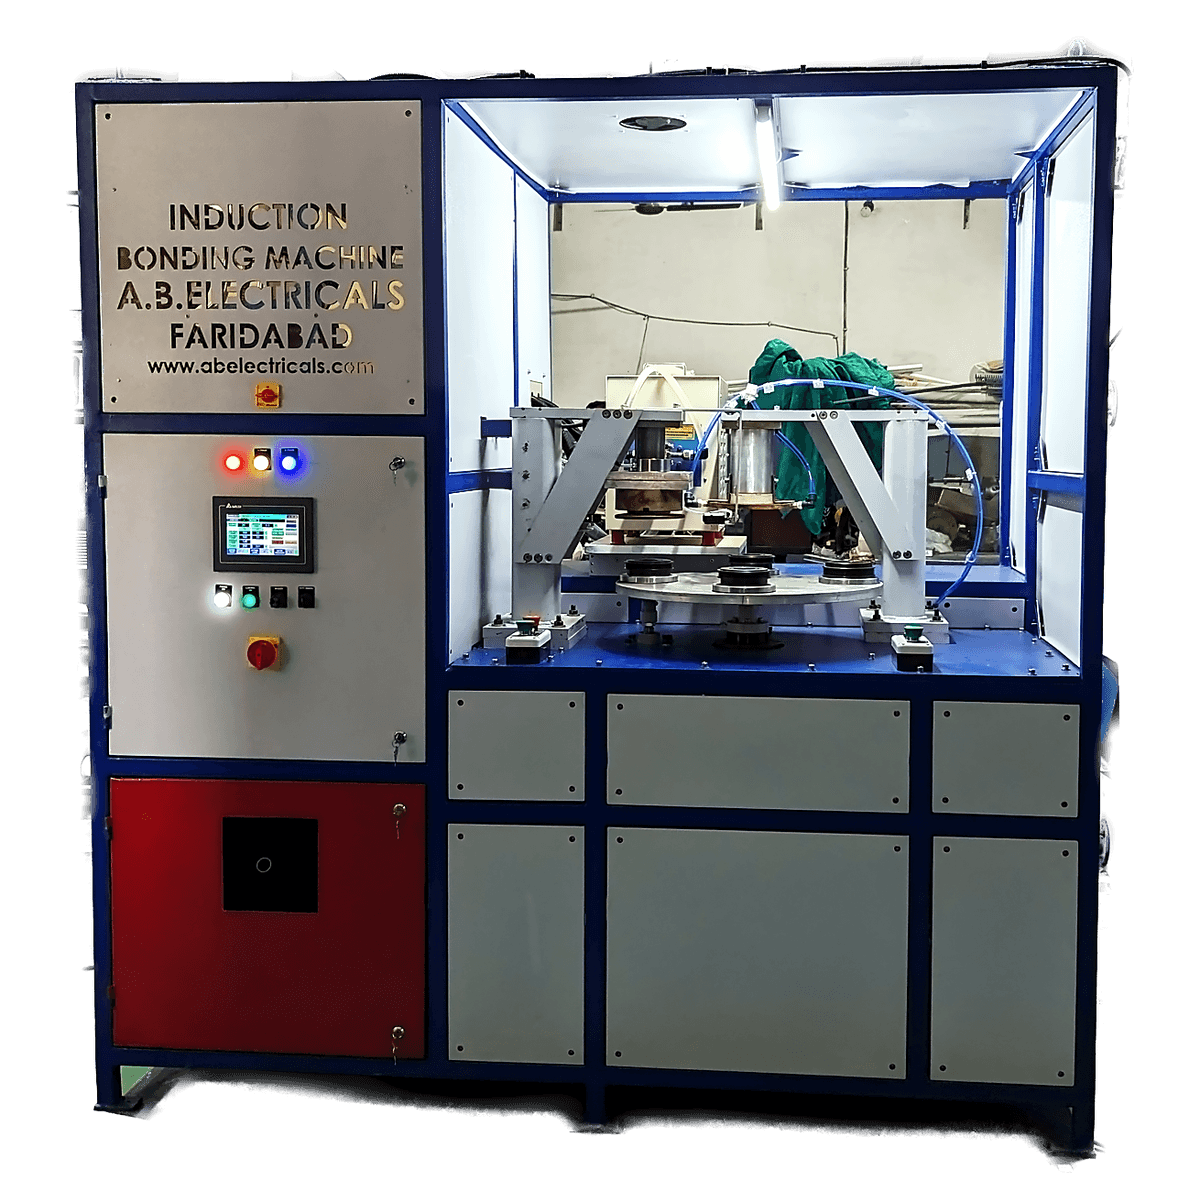
PLC based rotary induction bonding machine. 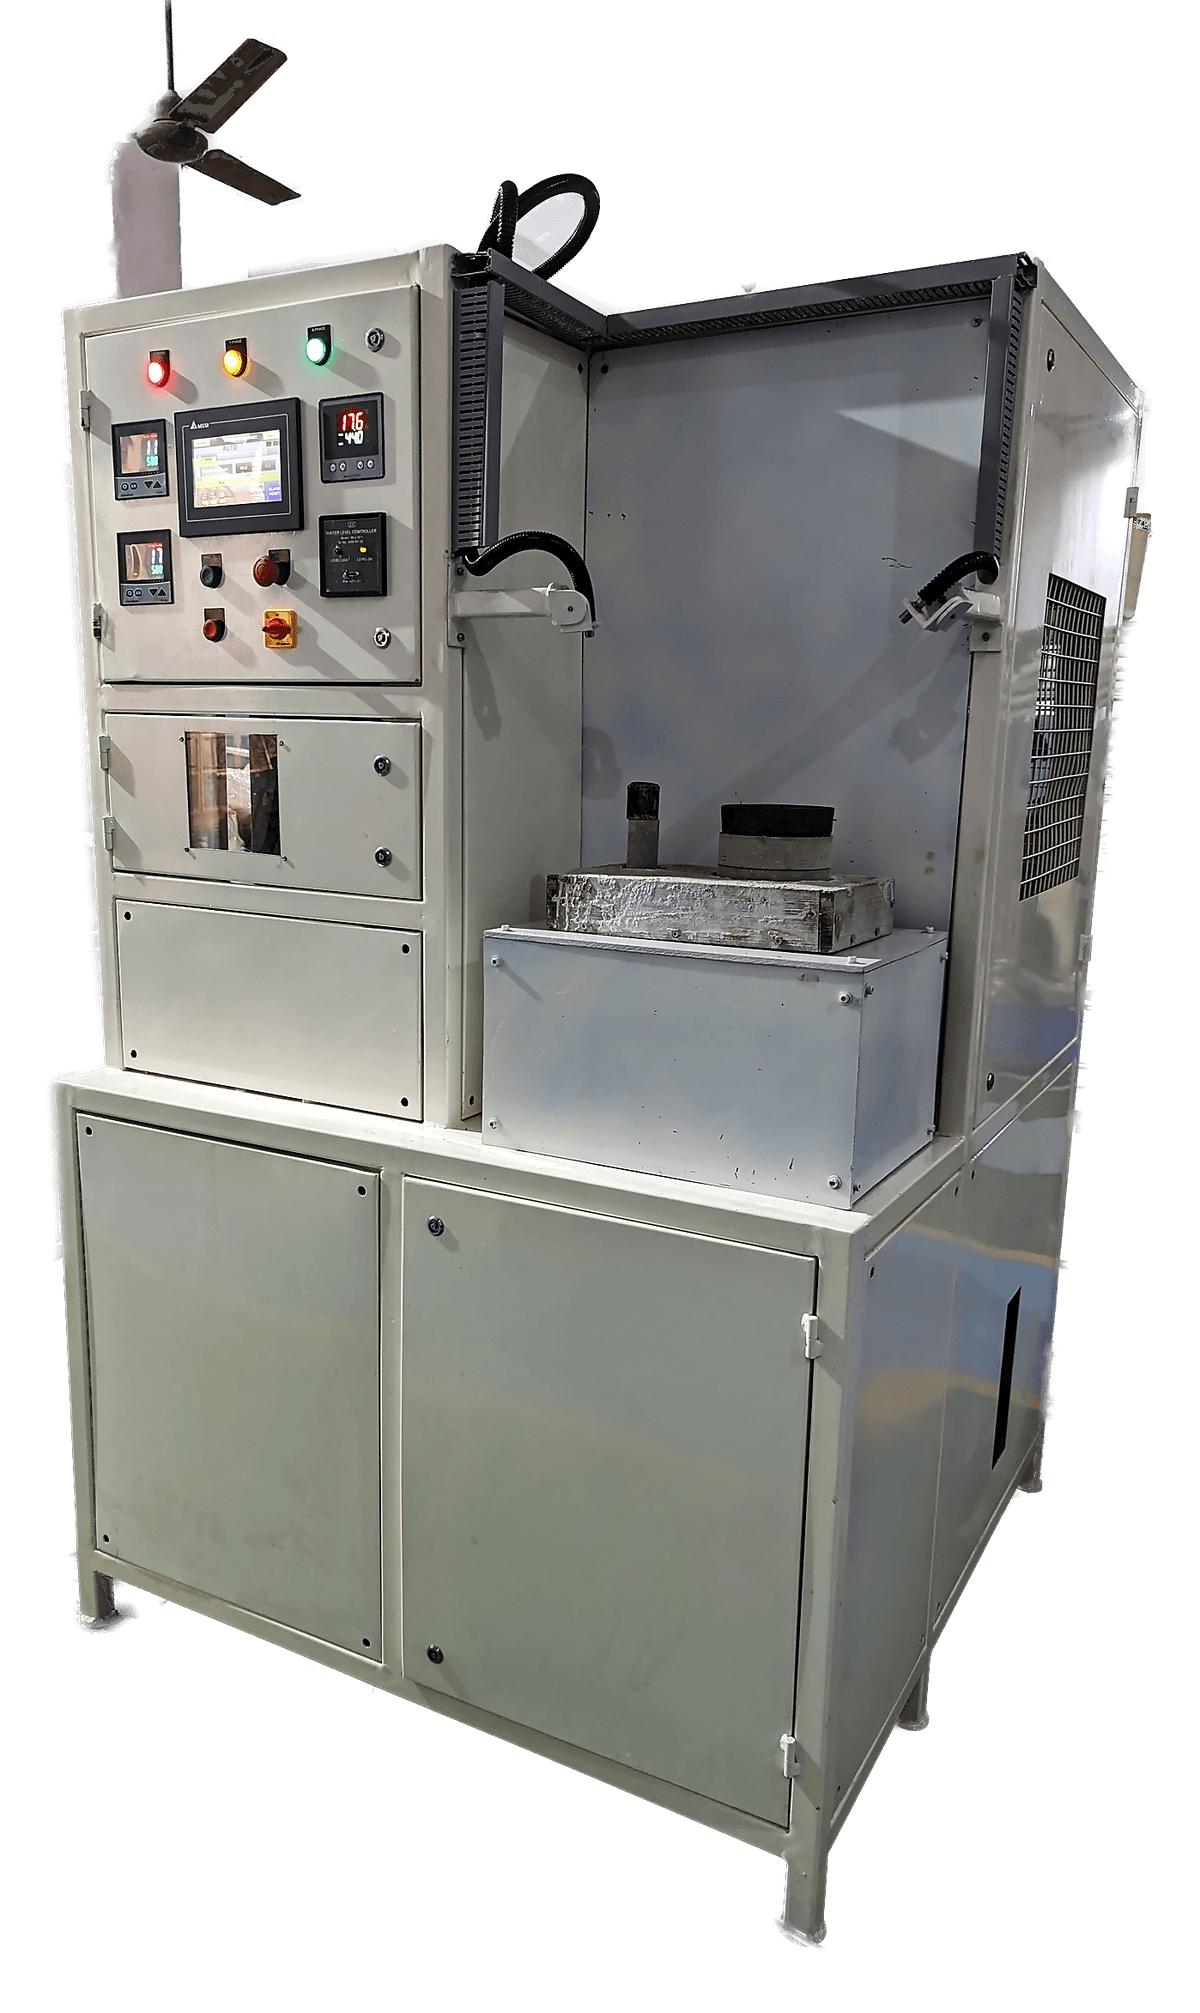
ABE-50AB CI ring and bush dual heating machine. 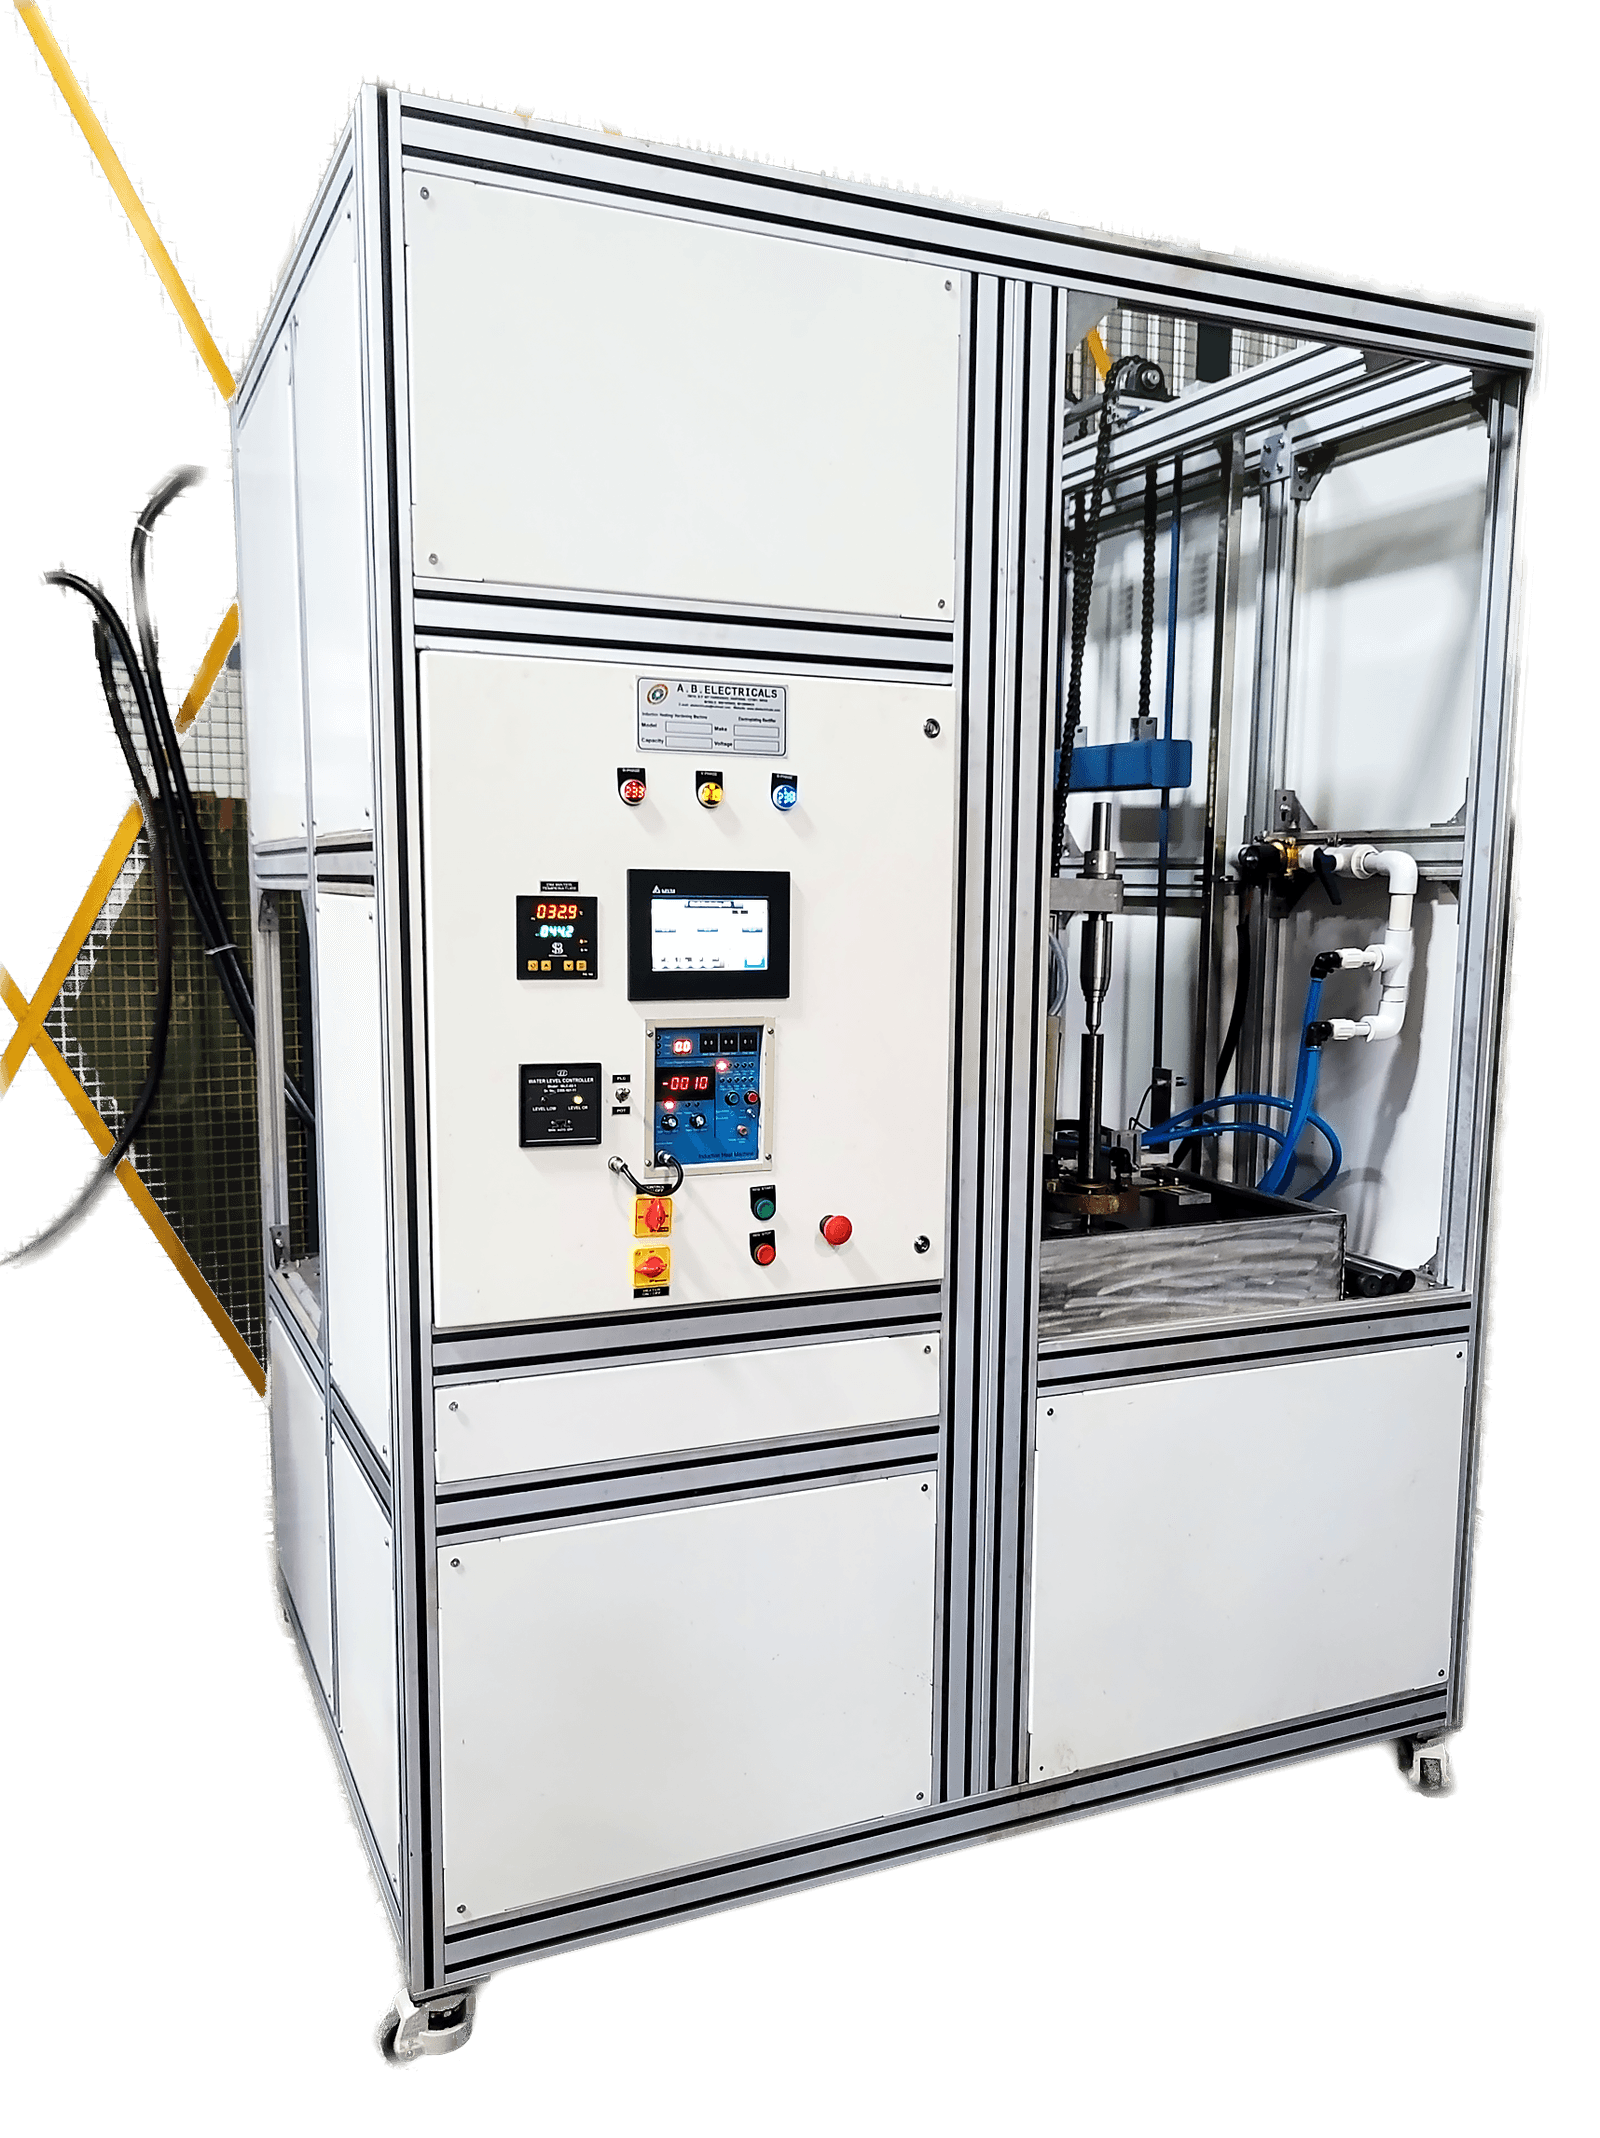
ABE-50AB axle shaft hardening machine. 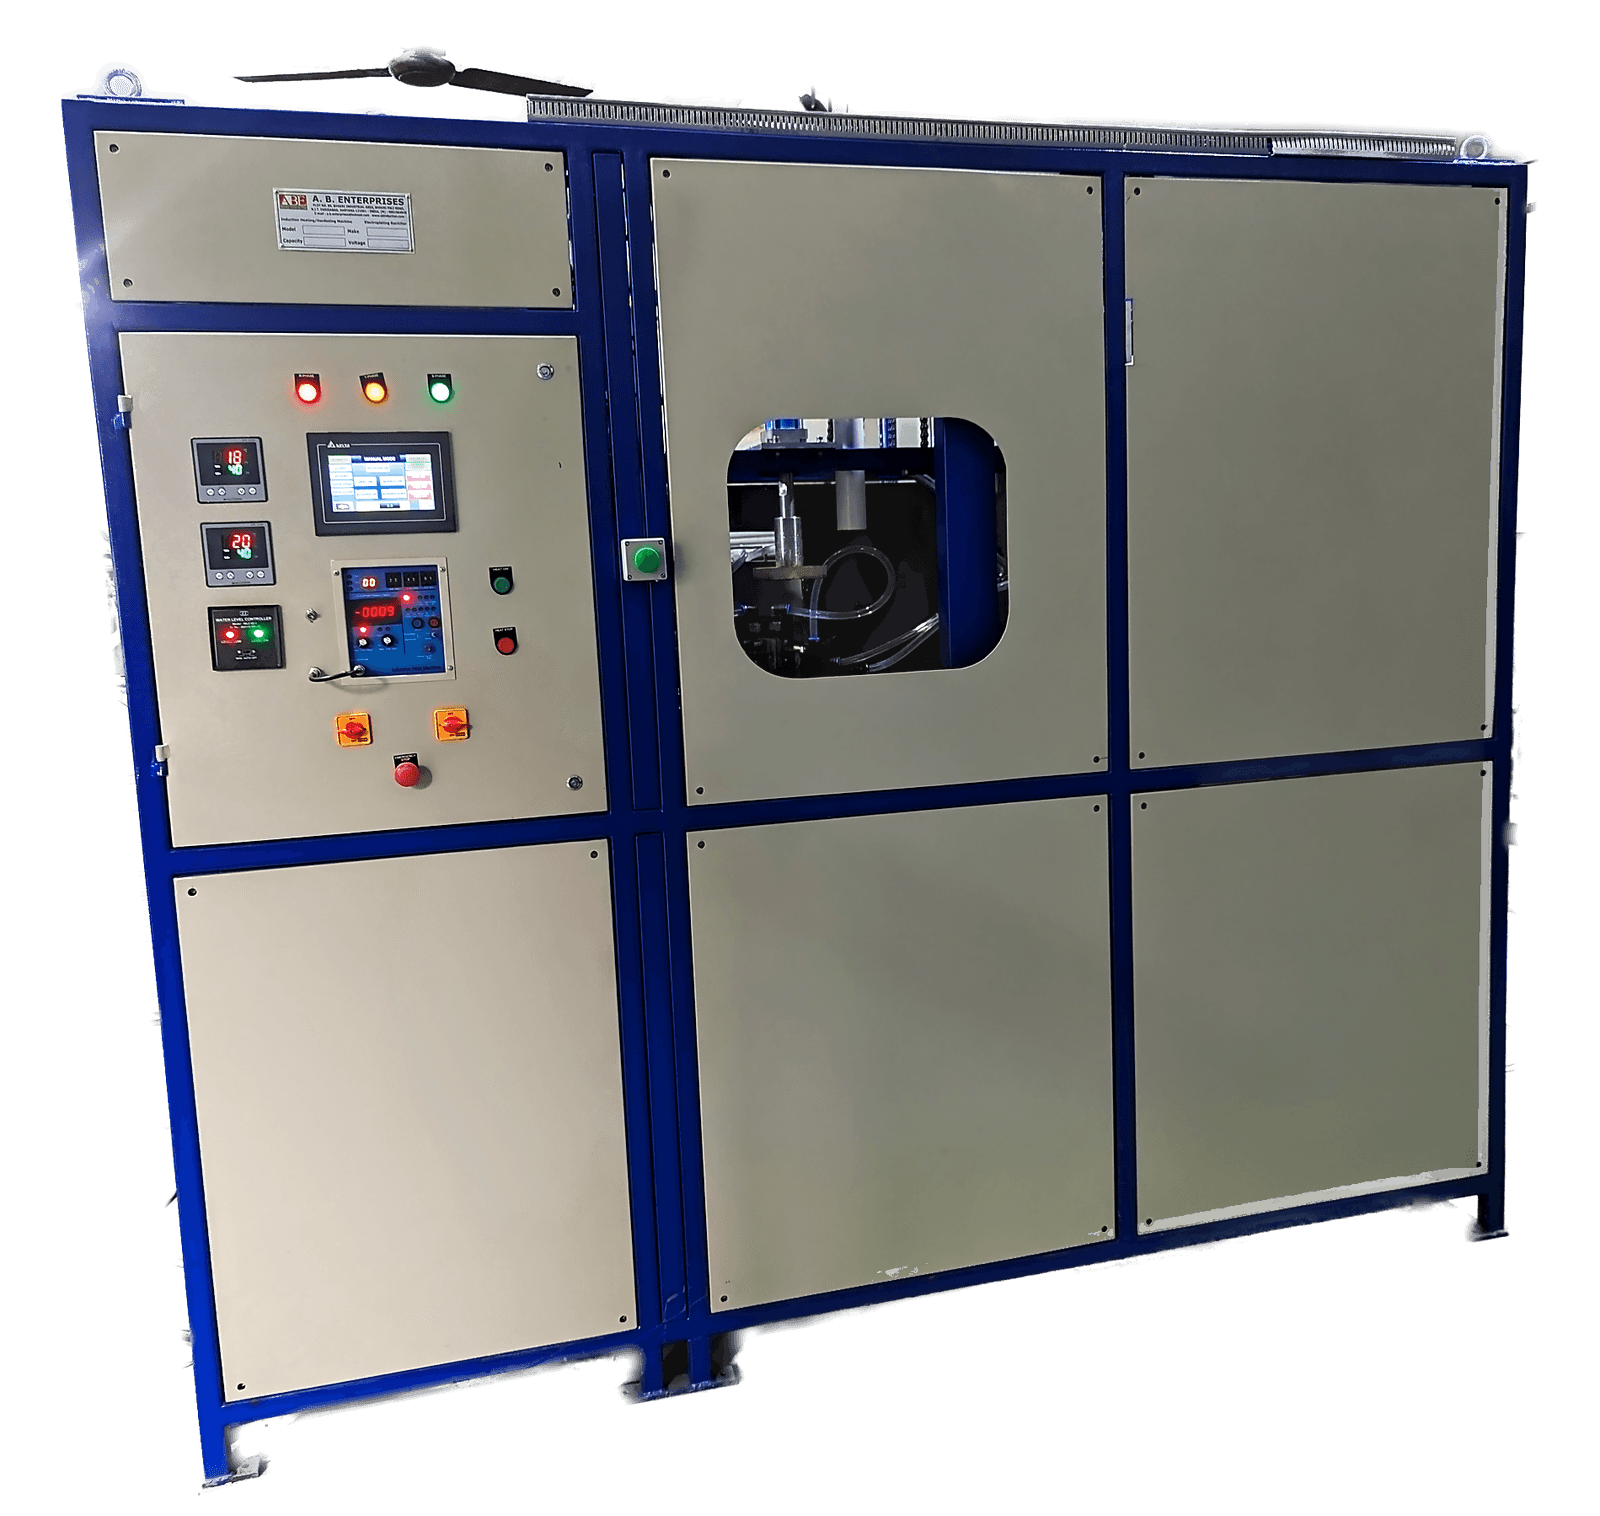
ABE-70AB induction hardening machine, 70 kW. 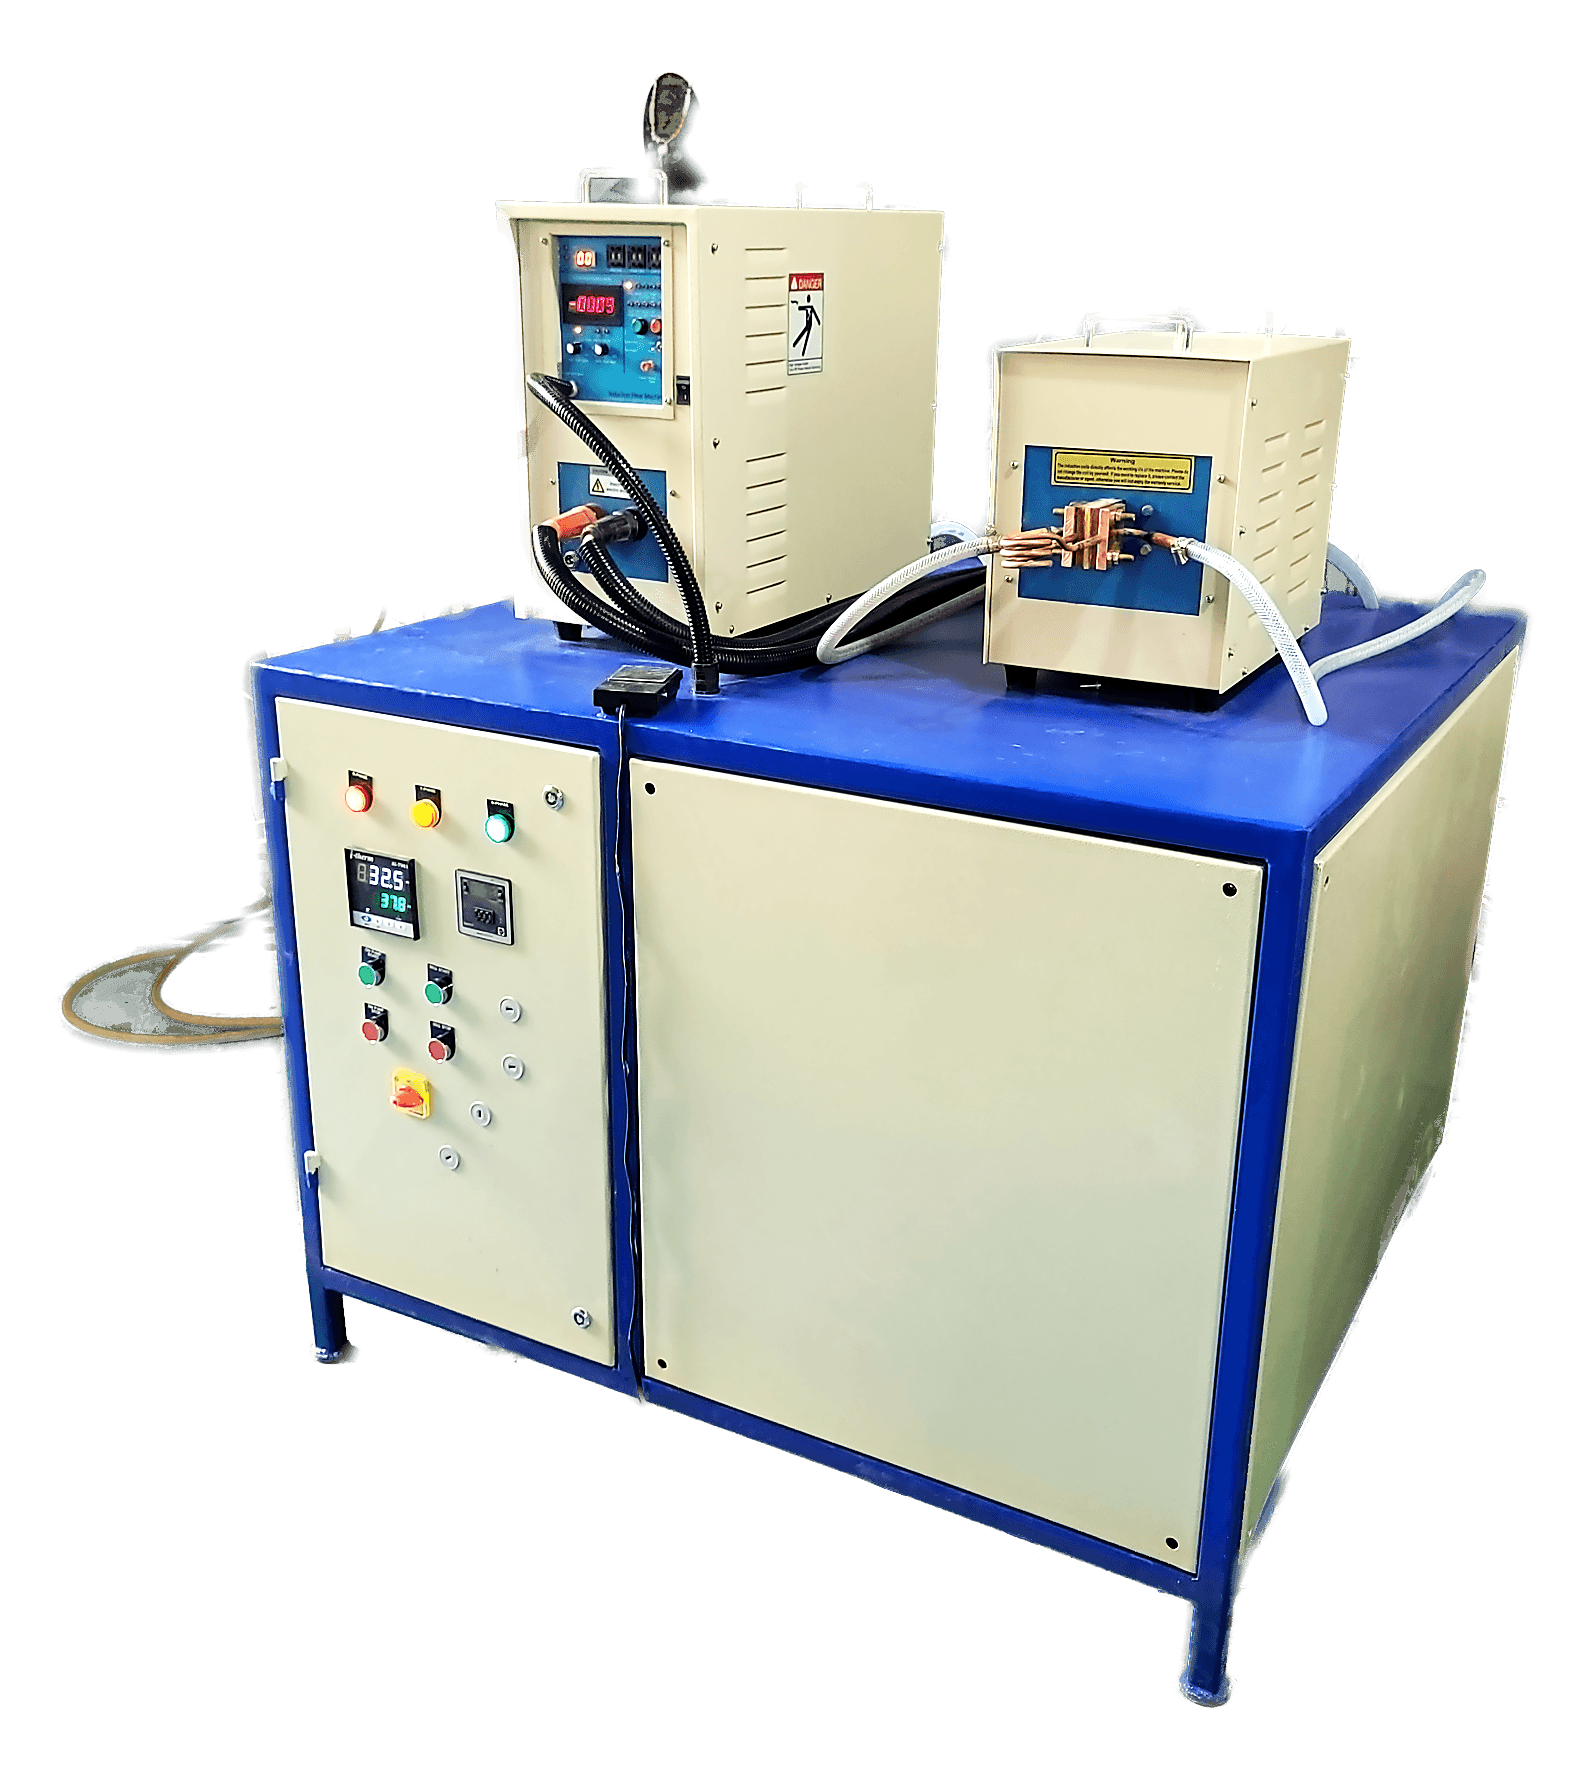
ABE-40AB induction heating machine, 40 kW. 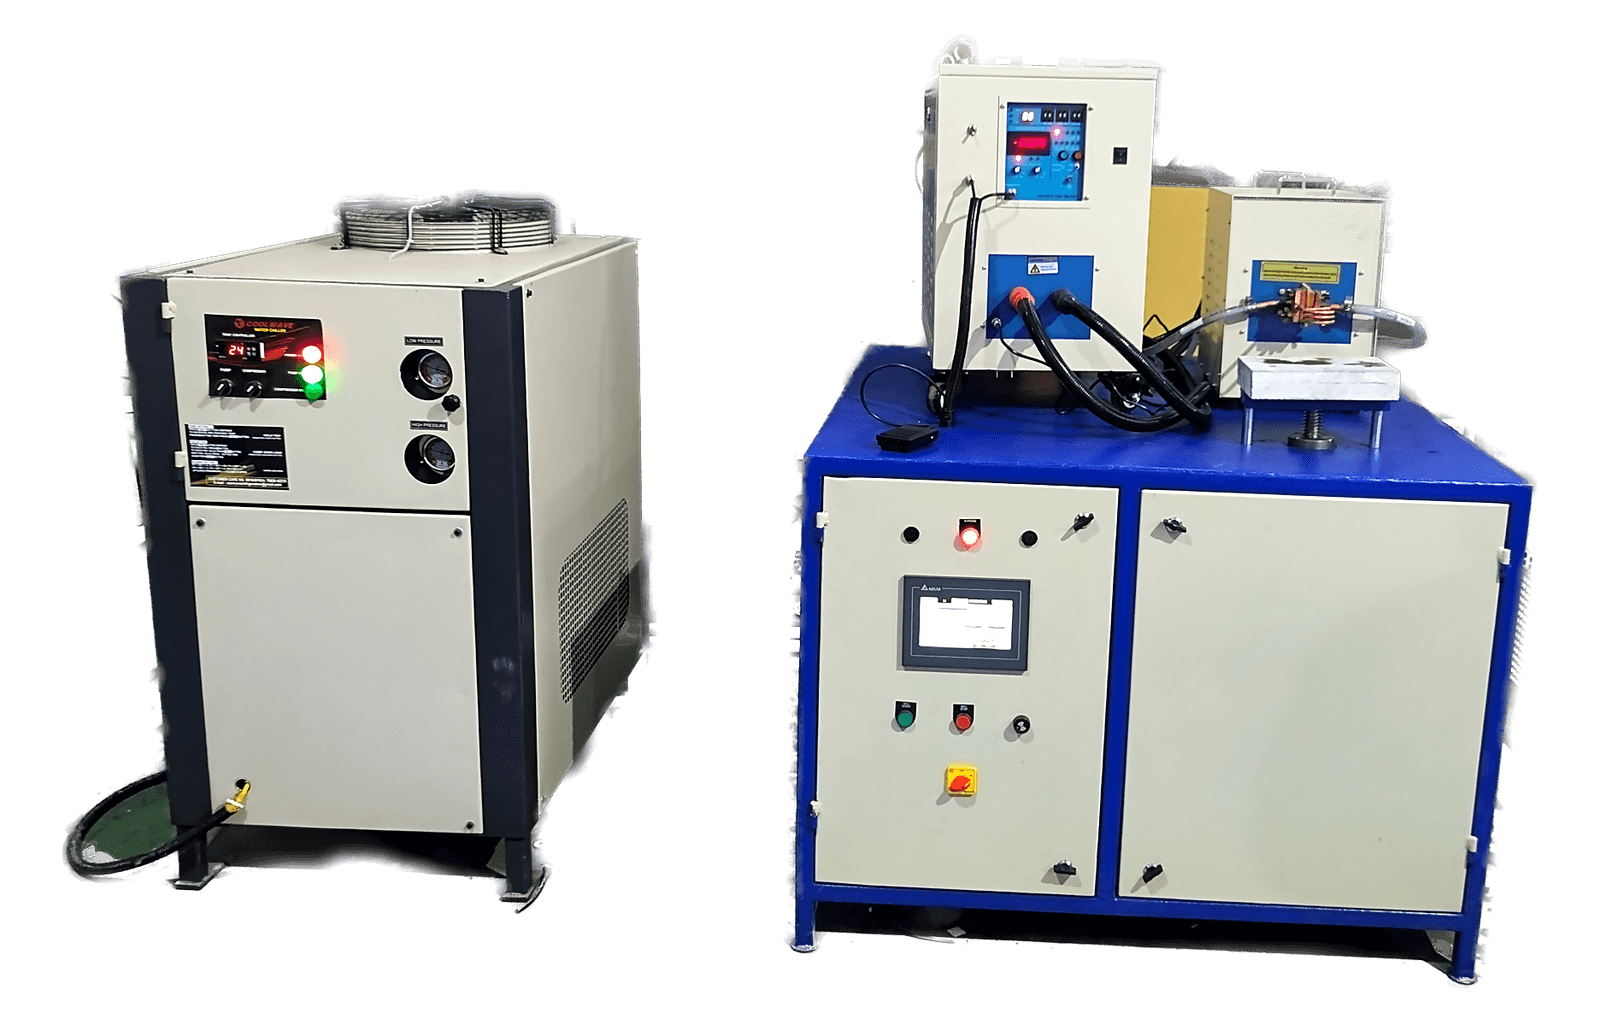
ABE-50AB supplied with a DM water chiller for continuous duty. 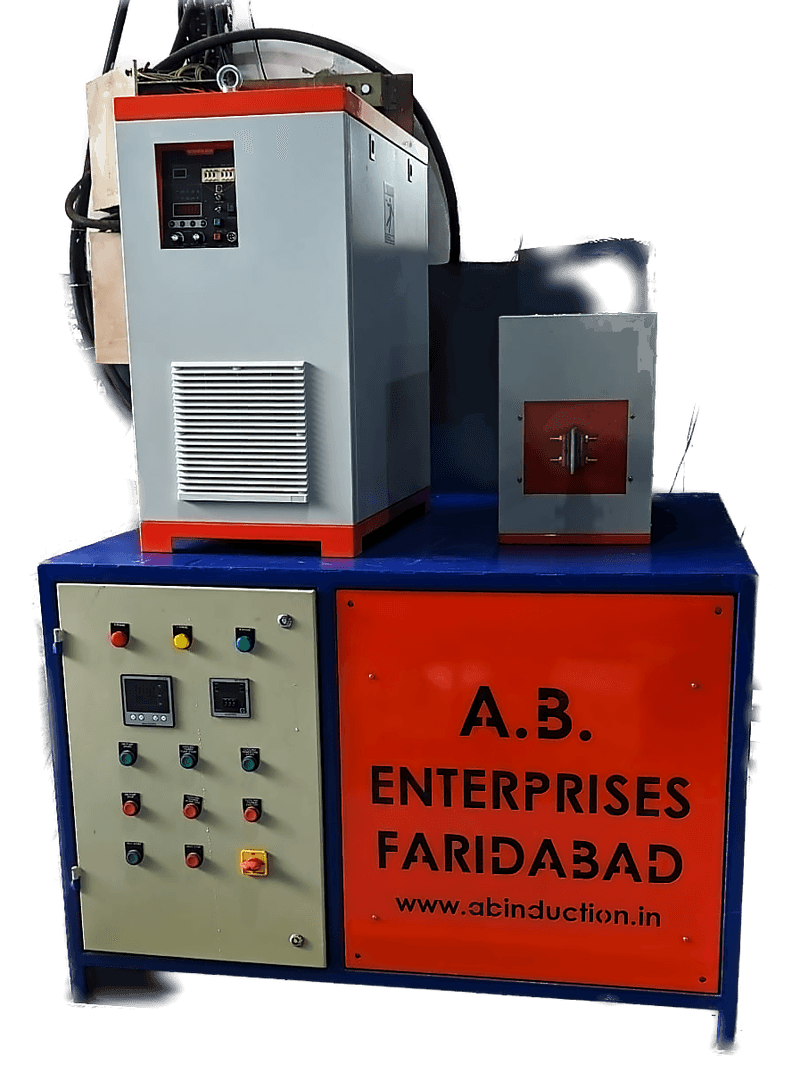
ABE-60AB ultra high frequency machine. 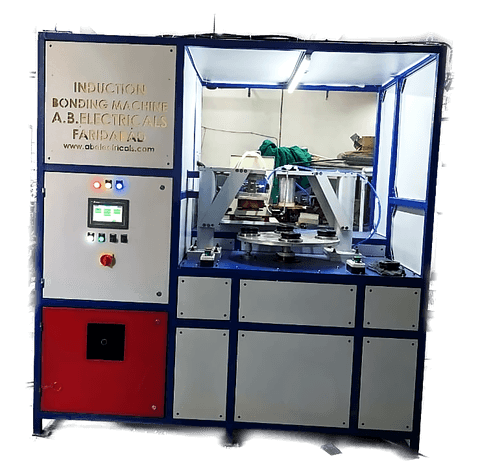
Induction bonding machine.
Inductors and parts at temperature
Coils are built in house, to the component. Several of these show steel actually at hardening or forging temperature.
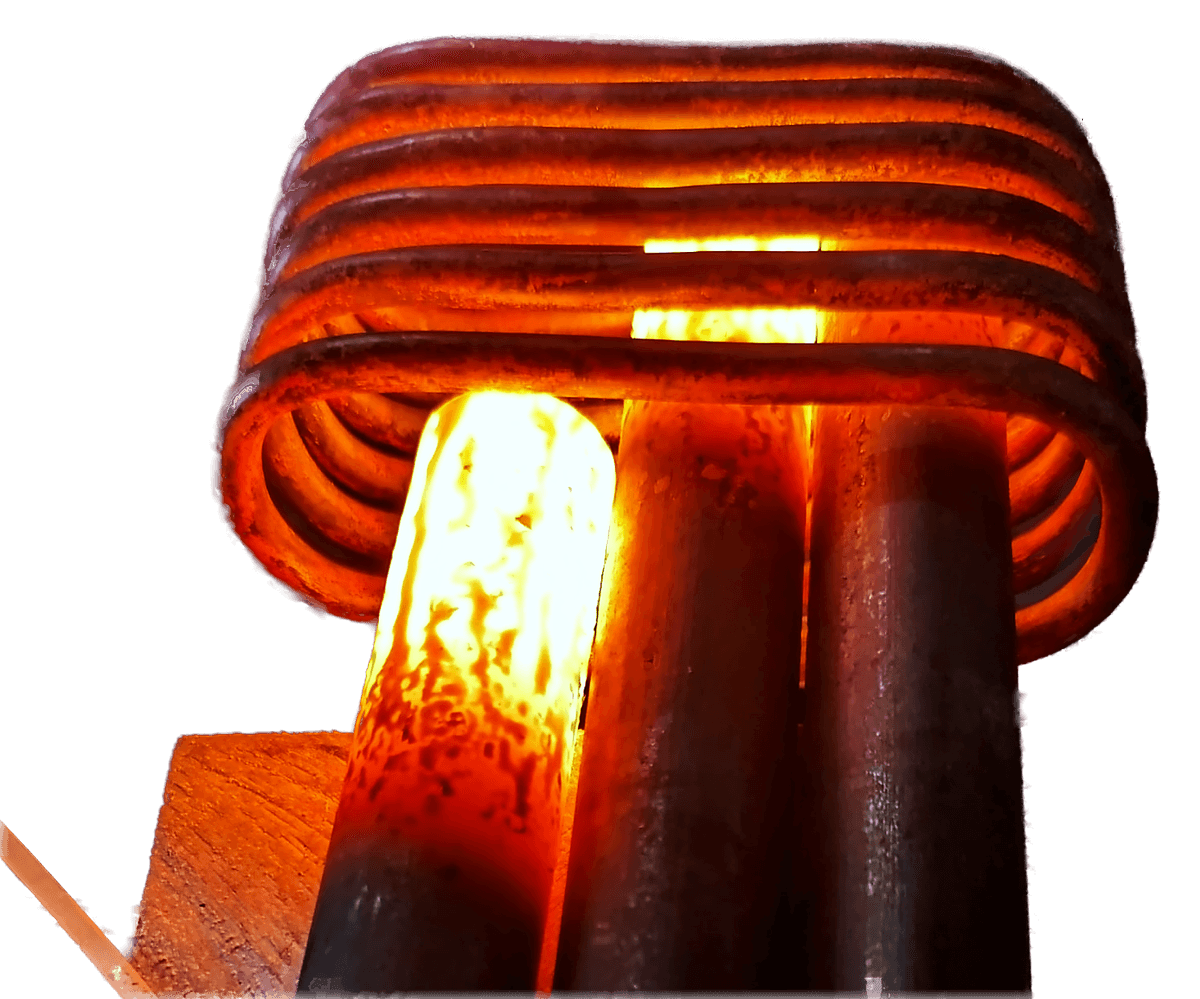
Bar end heating. Only the bar is hot. 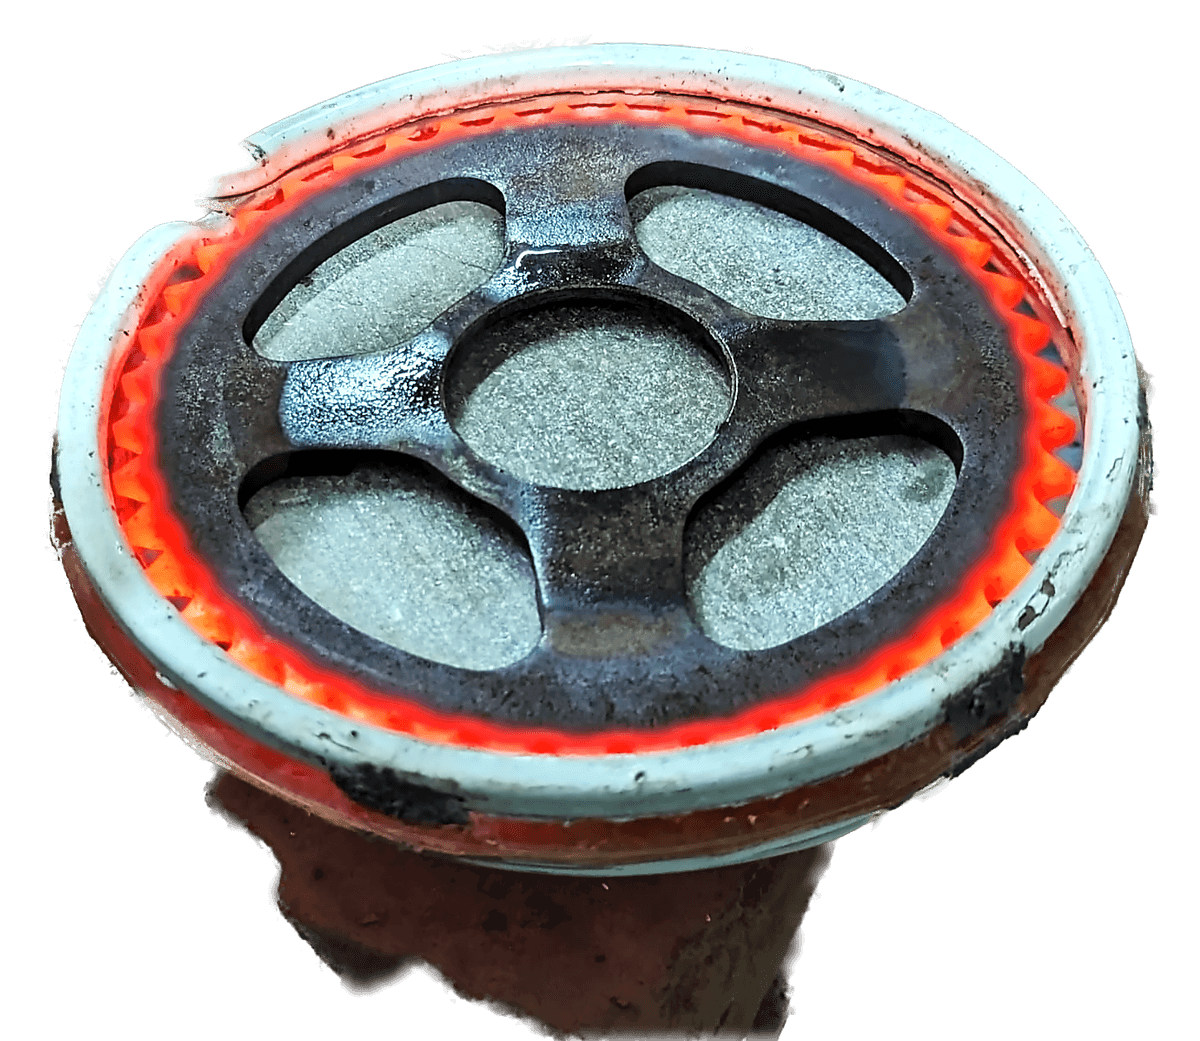
A ring gear at temperature, glowing evenly all the way round. 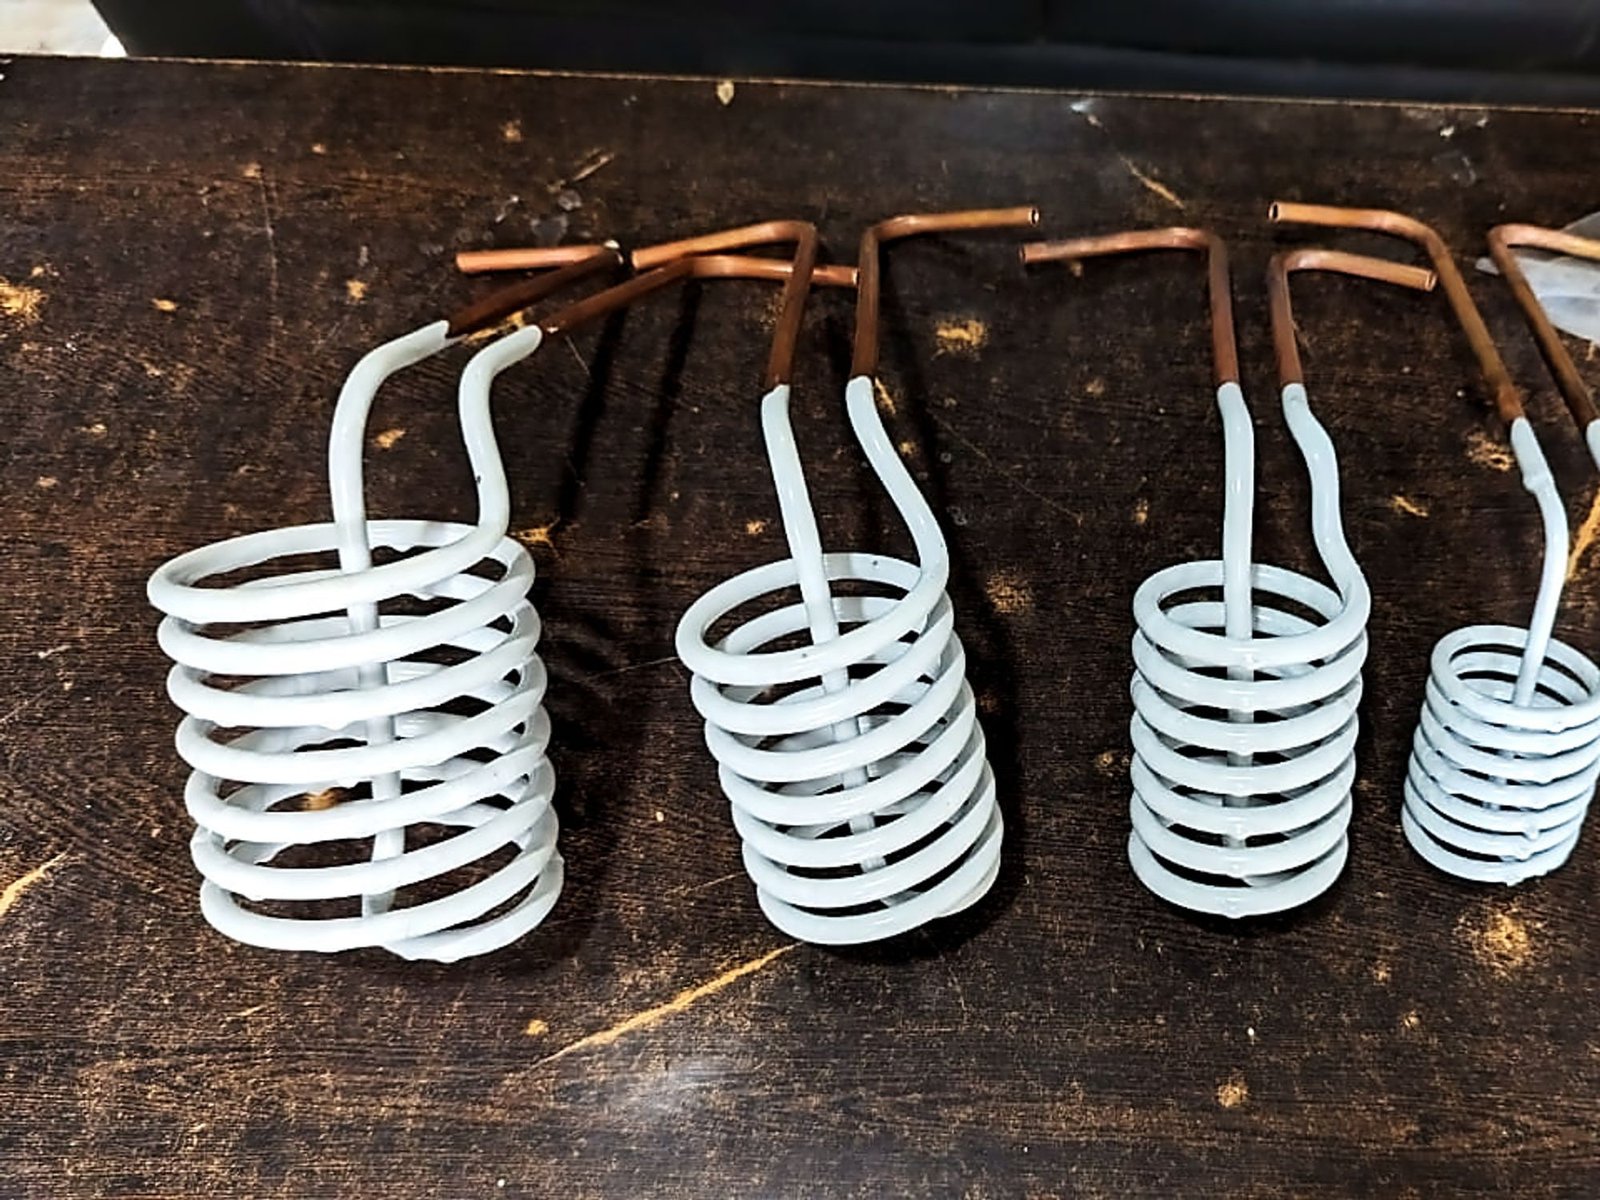
Four inductors, four different components. 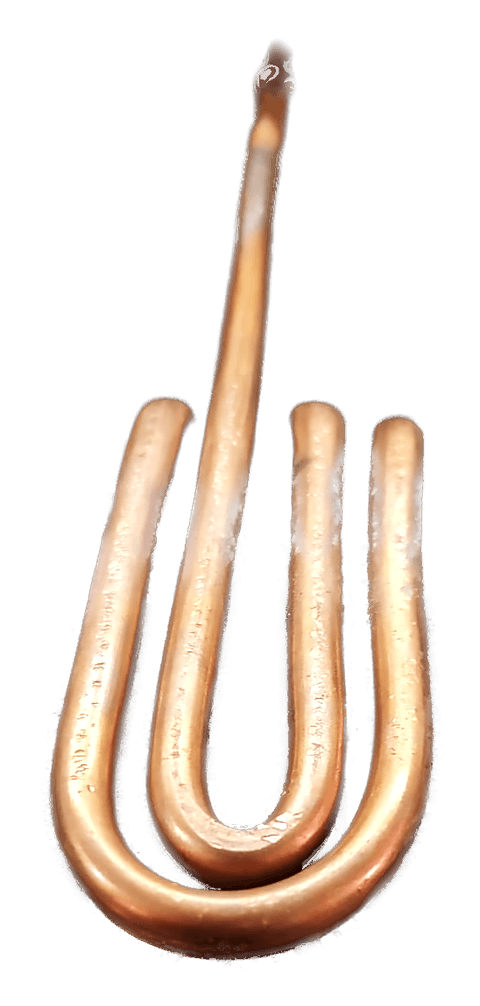
A hairpin inductor over a forged part. 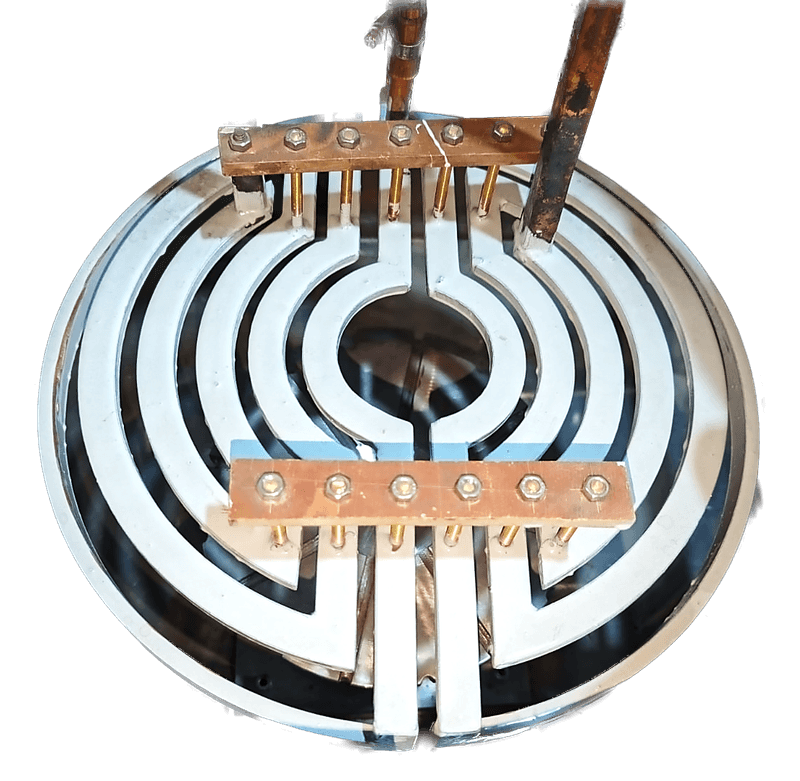
A pancake inductor, for heating a flat face. 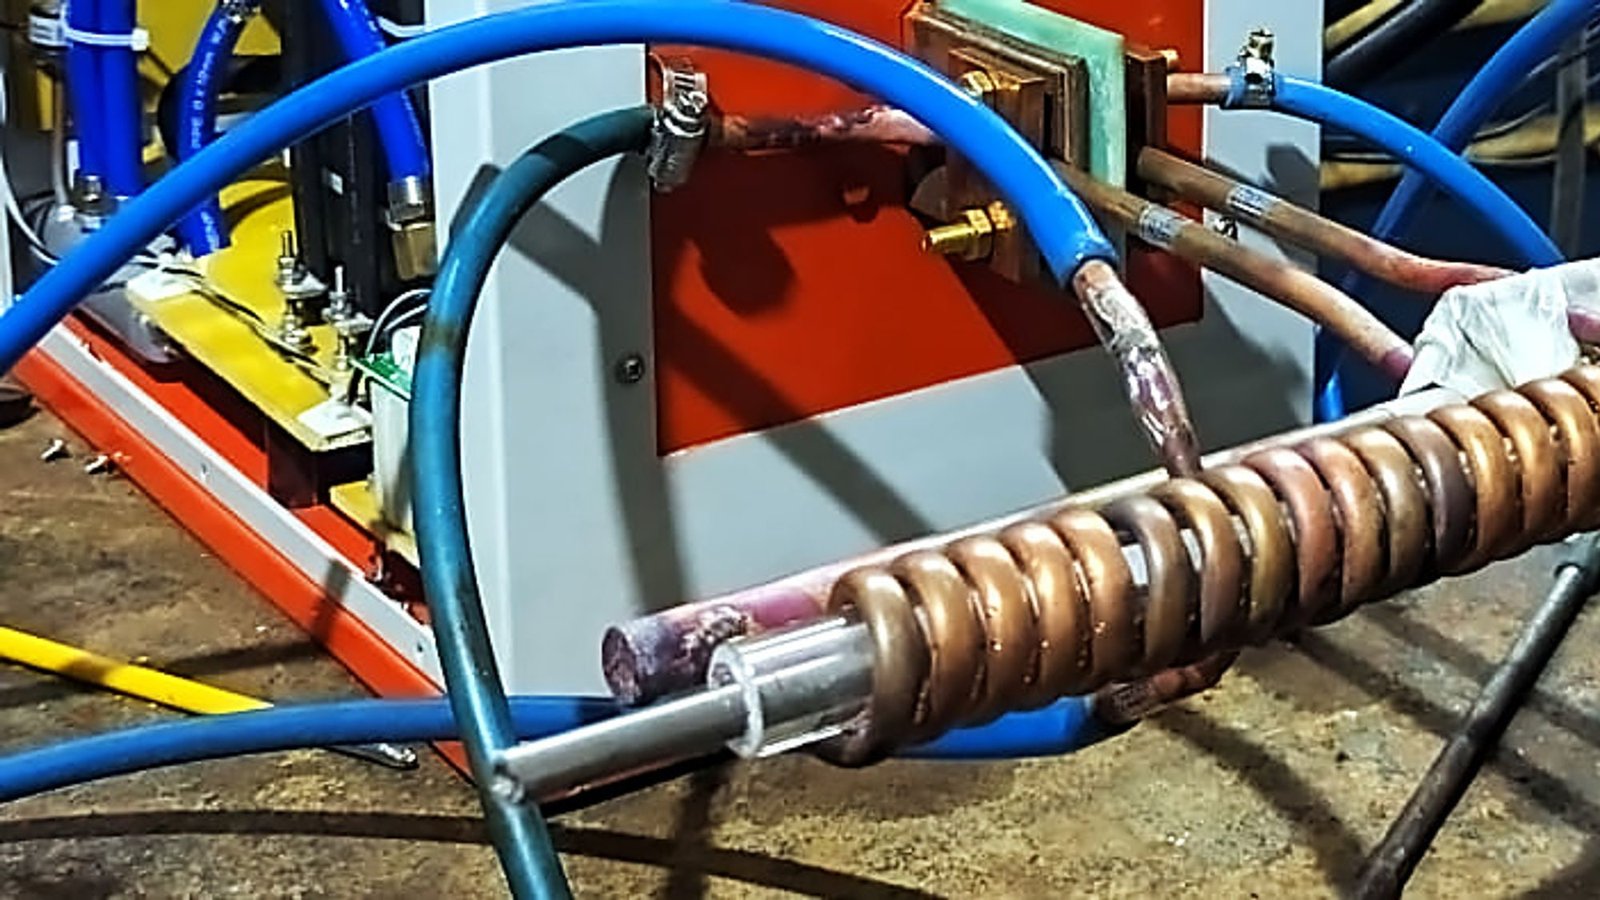
Coil fabrication in the workshop. 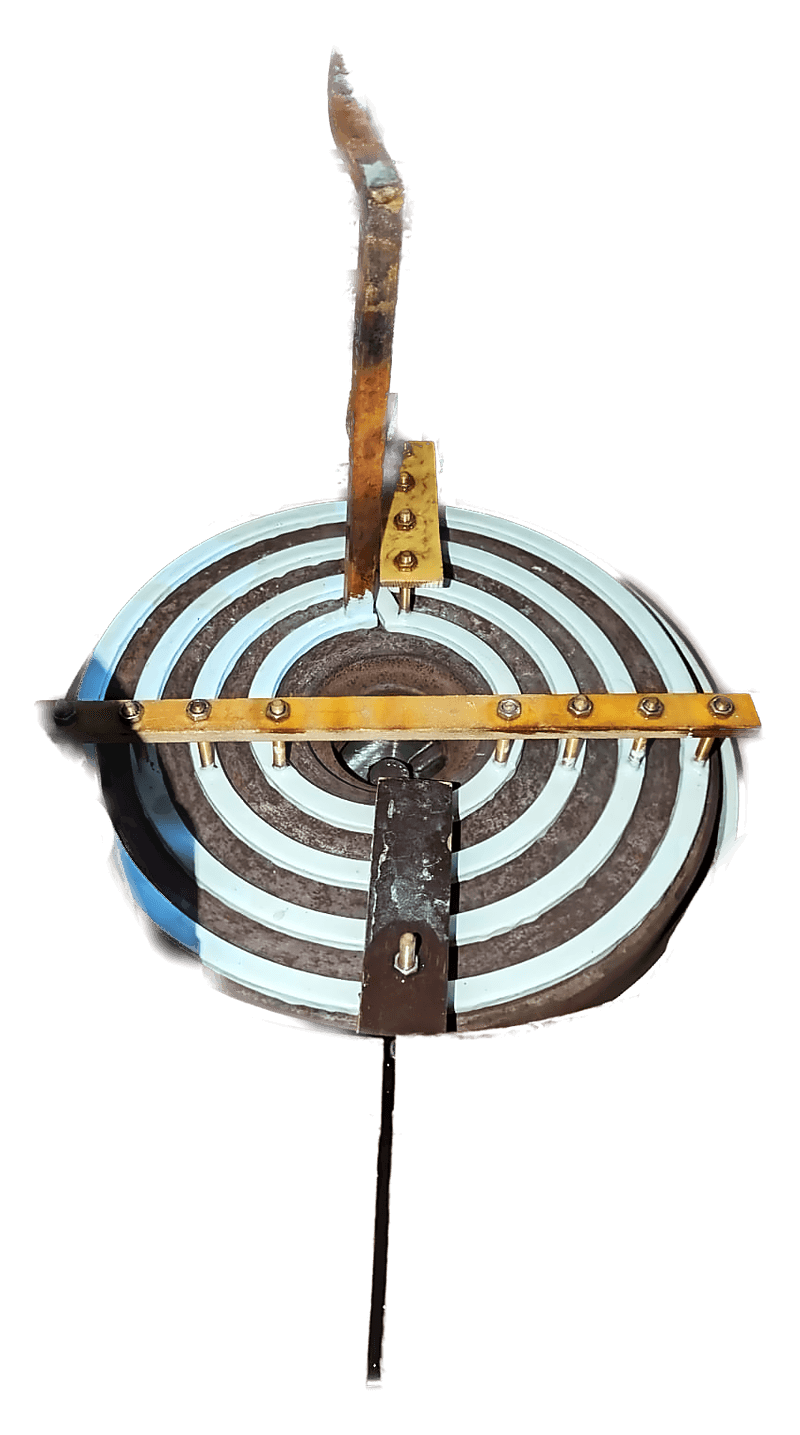
A pancake inductor inside its copper enclosure. 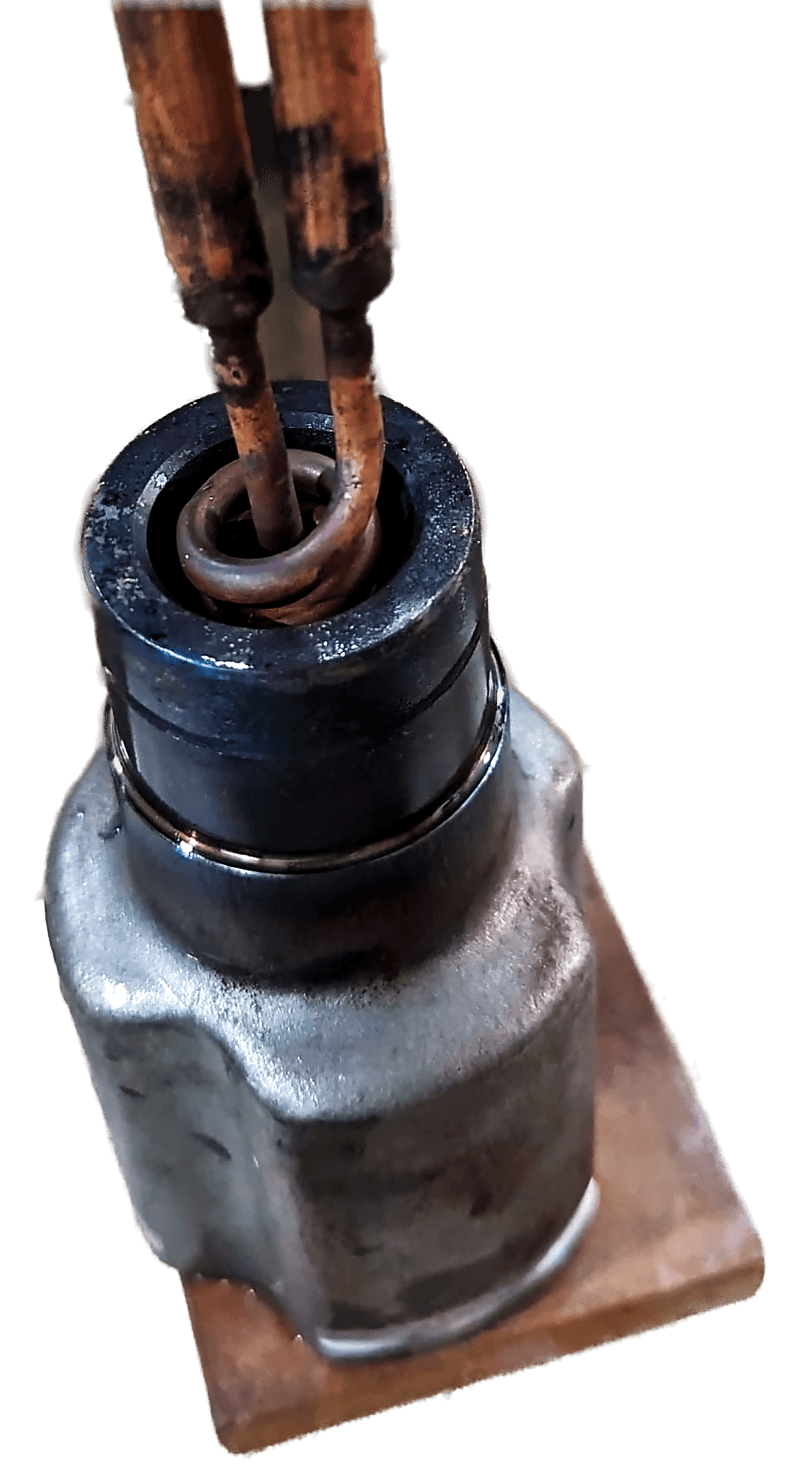
An encircling coil around a cylindrical part. 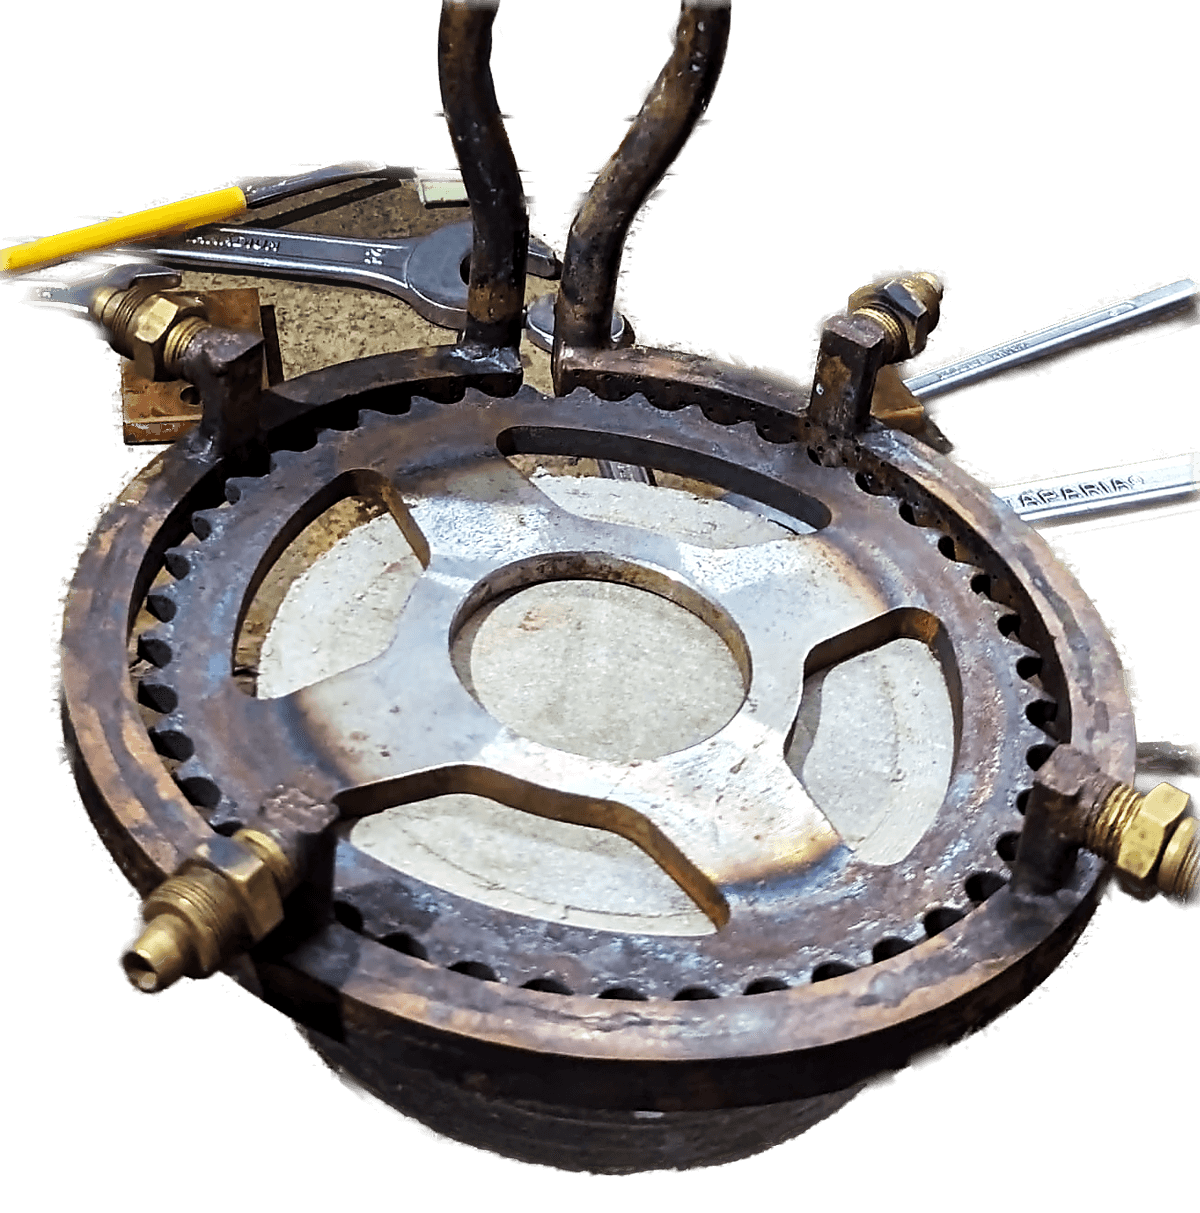
A ring gear before treatment. 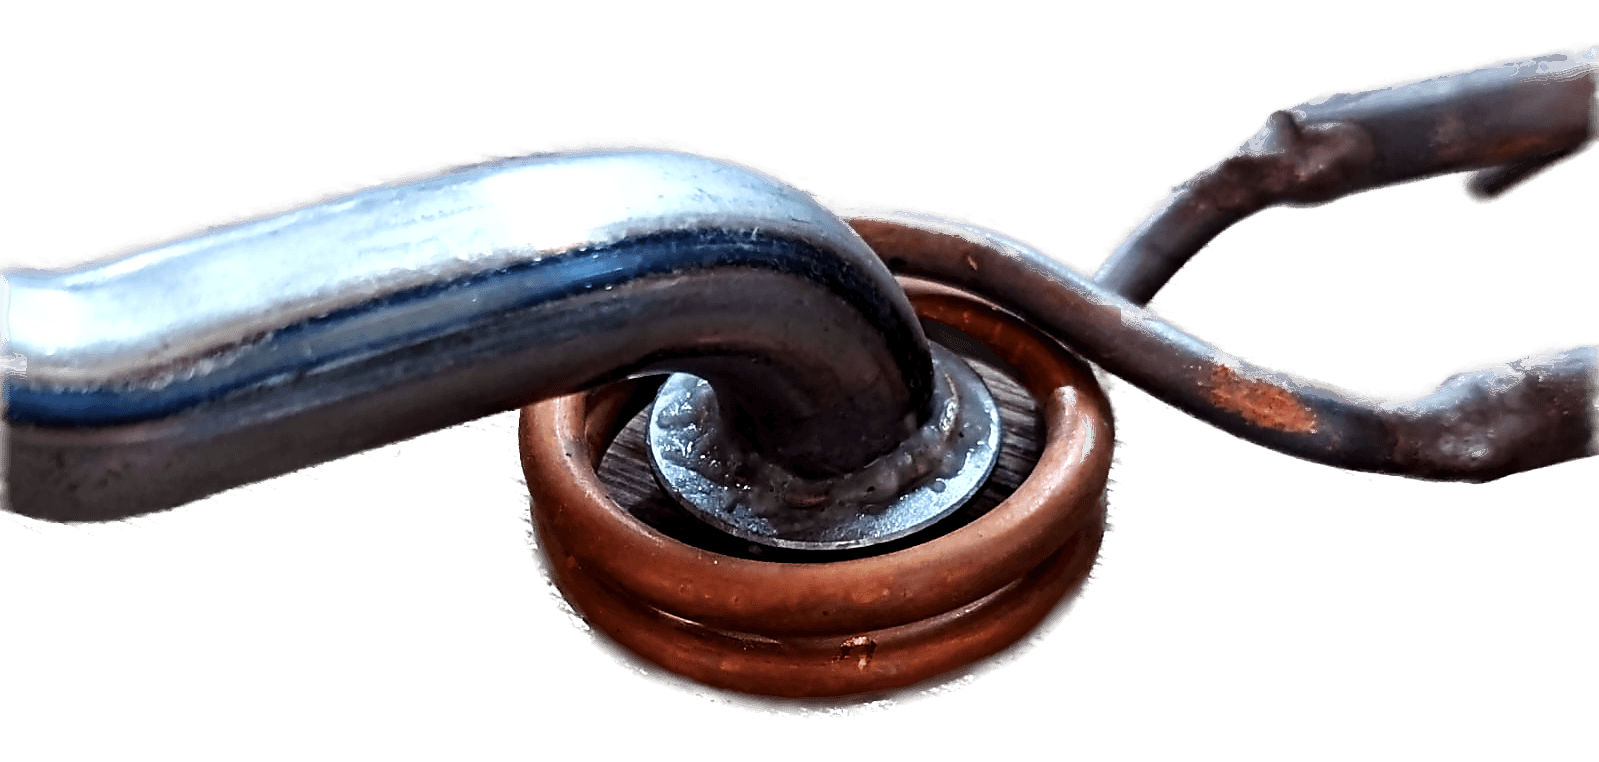
A small close-coupled coil. 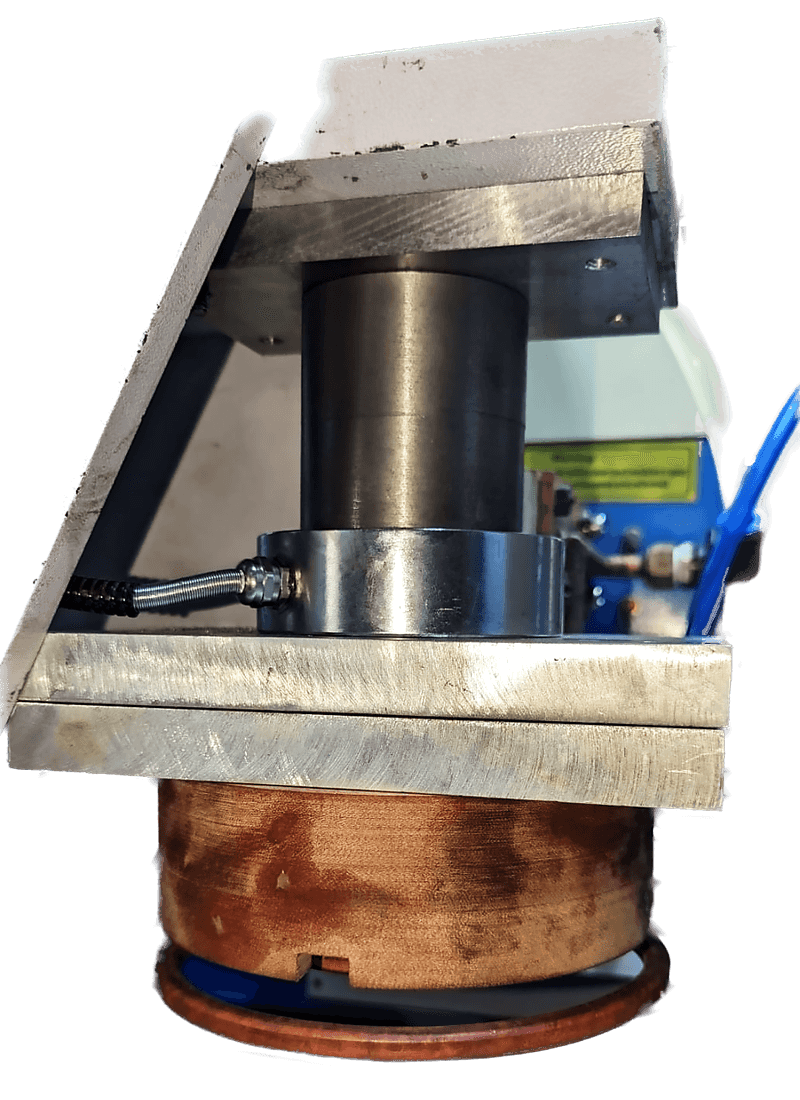
A ring inductor built into a station. 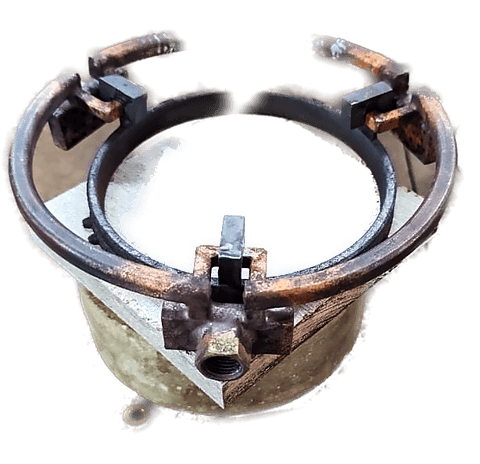
Coil, clamps and workpiece location as one assembly.
Our team
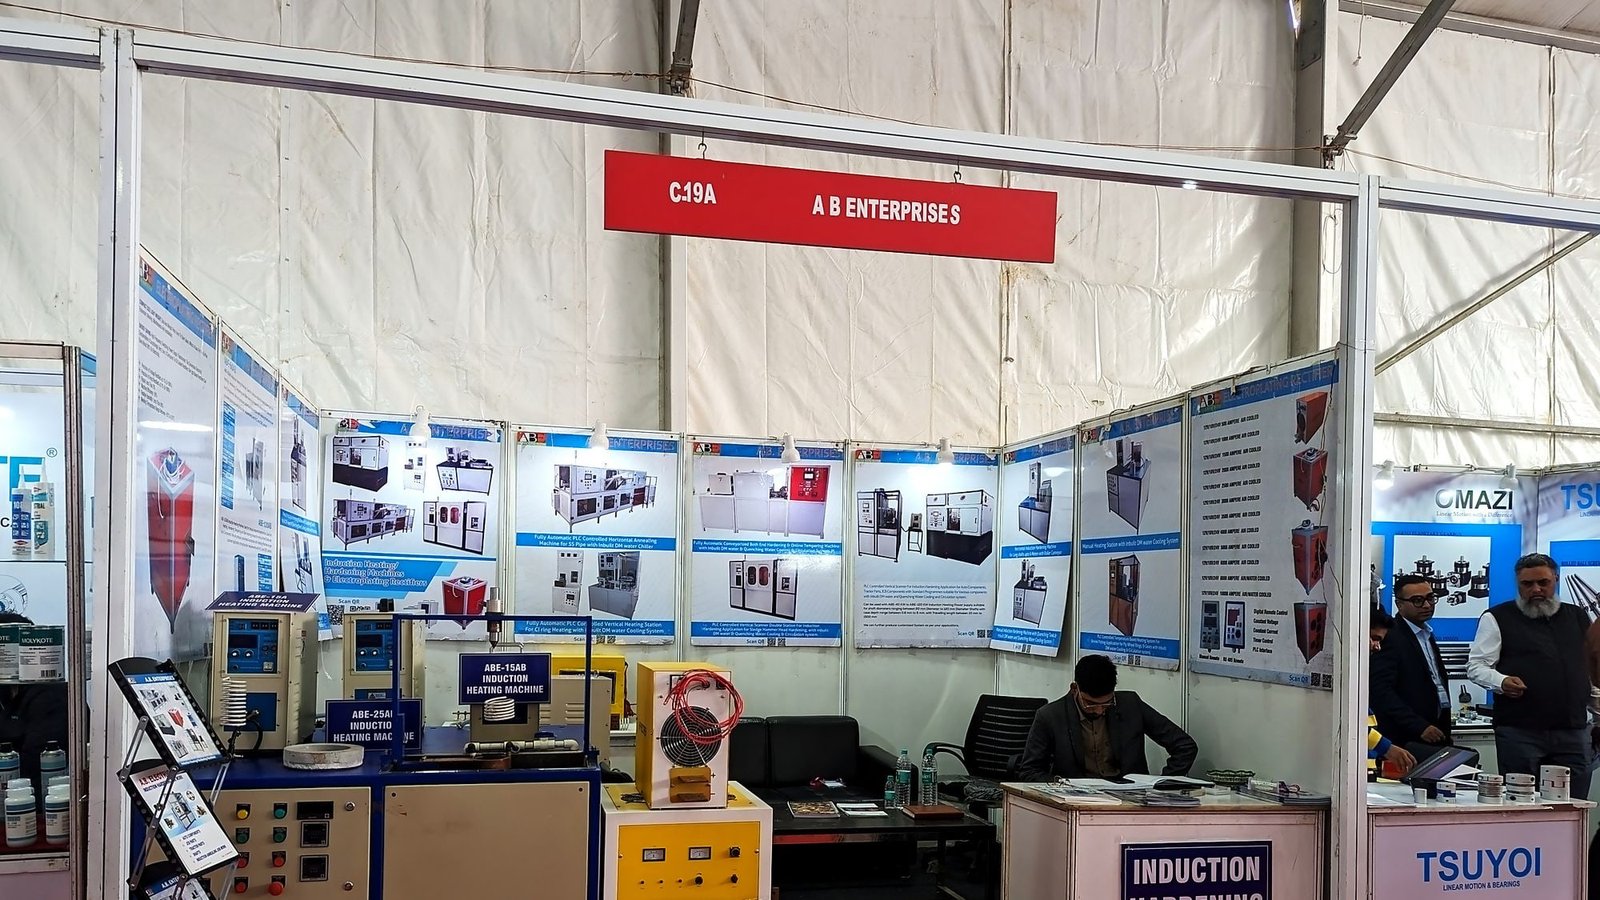
Our team and equipment at an industry exhibition. 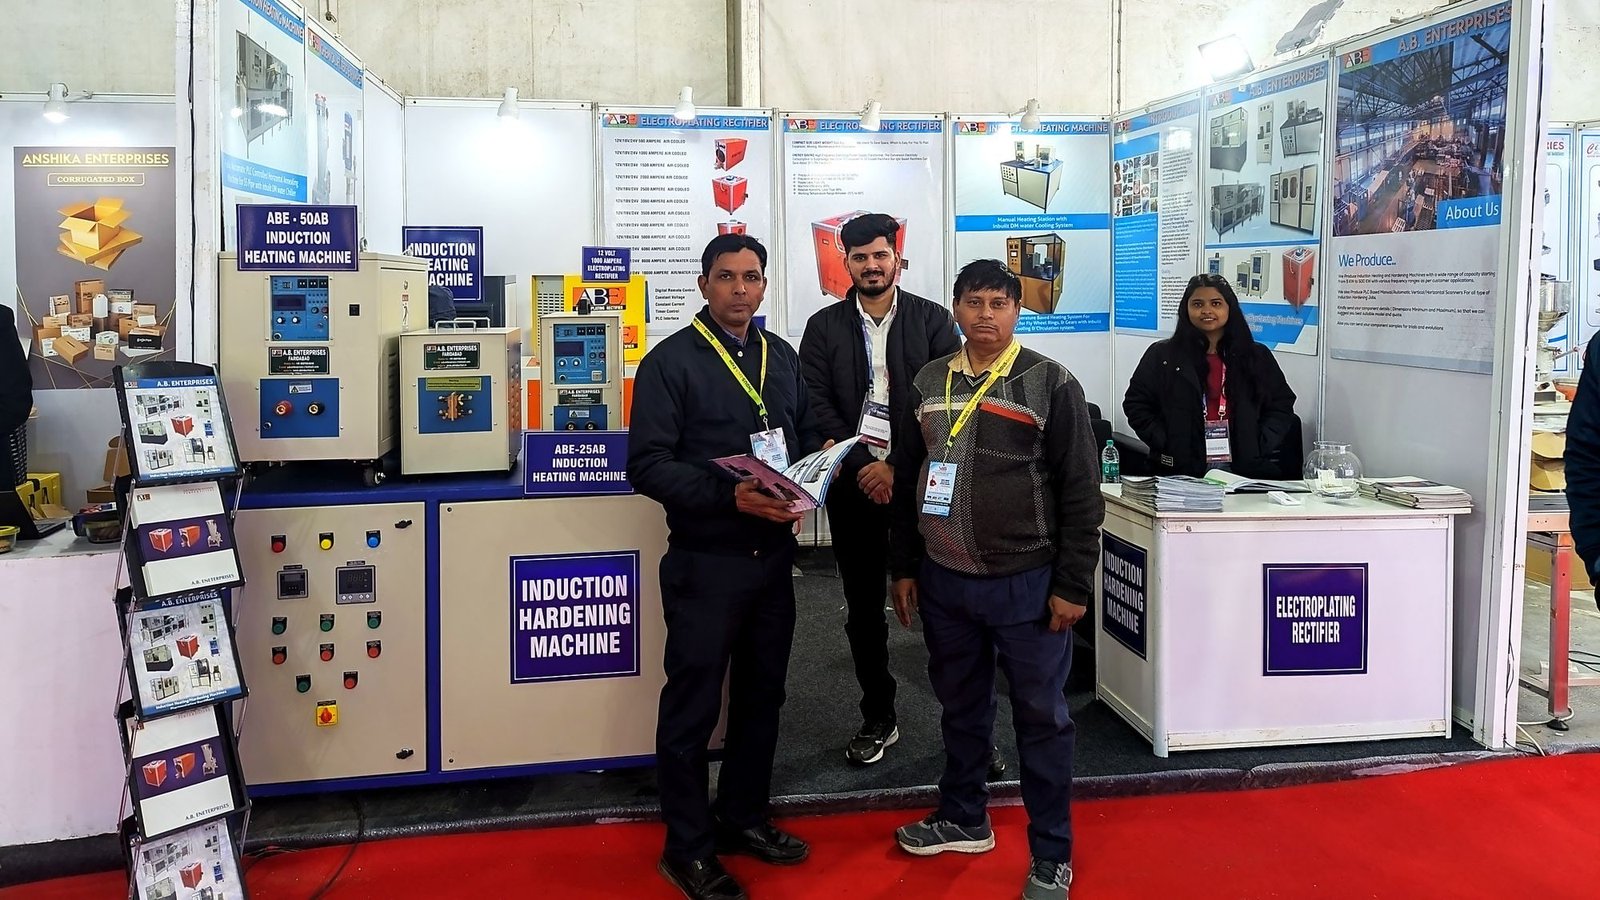
The stand, showing induction and plating equipment together.
Tell us about the part.
Send a drawing, the material, the case depth or temperature you need, and your production rate. Our engineers will help define the right machine for your process.