
Case studies
Explore four machines we have built for flywheel rings, hammer heads, axle shafts and CI ring pre-heating. Each started with a specific component and production requirement.
See how we approached the coil, machine layout and process for each component.
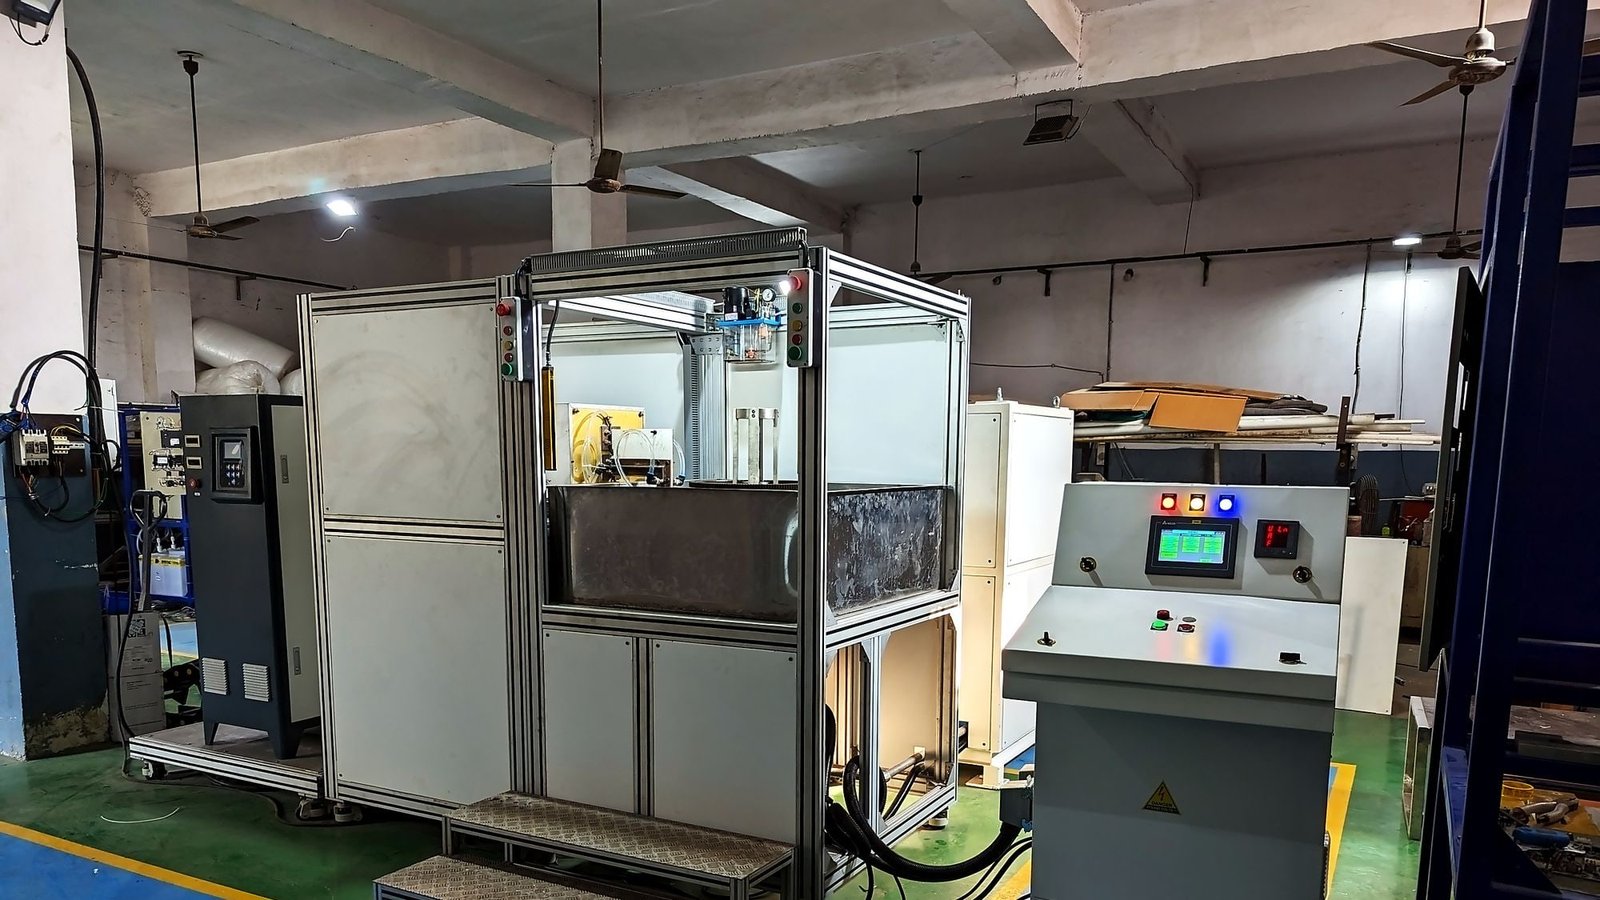
Flywheel starter ring hardening at 120 kW
Hardening a starter ring gear all the way round, at consistent depth.
- Machine applicationInduction hardening
Sledge hammer head hardening, double station
Two stations, because the operator was the bottleneck and not the heat.
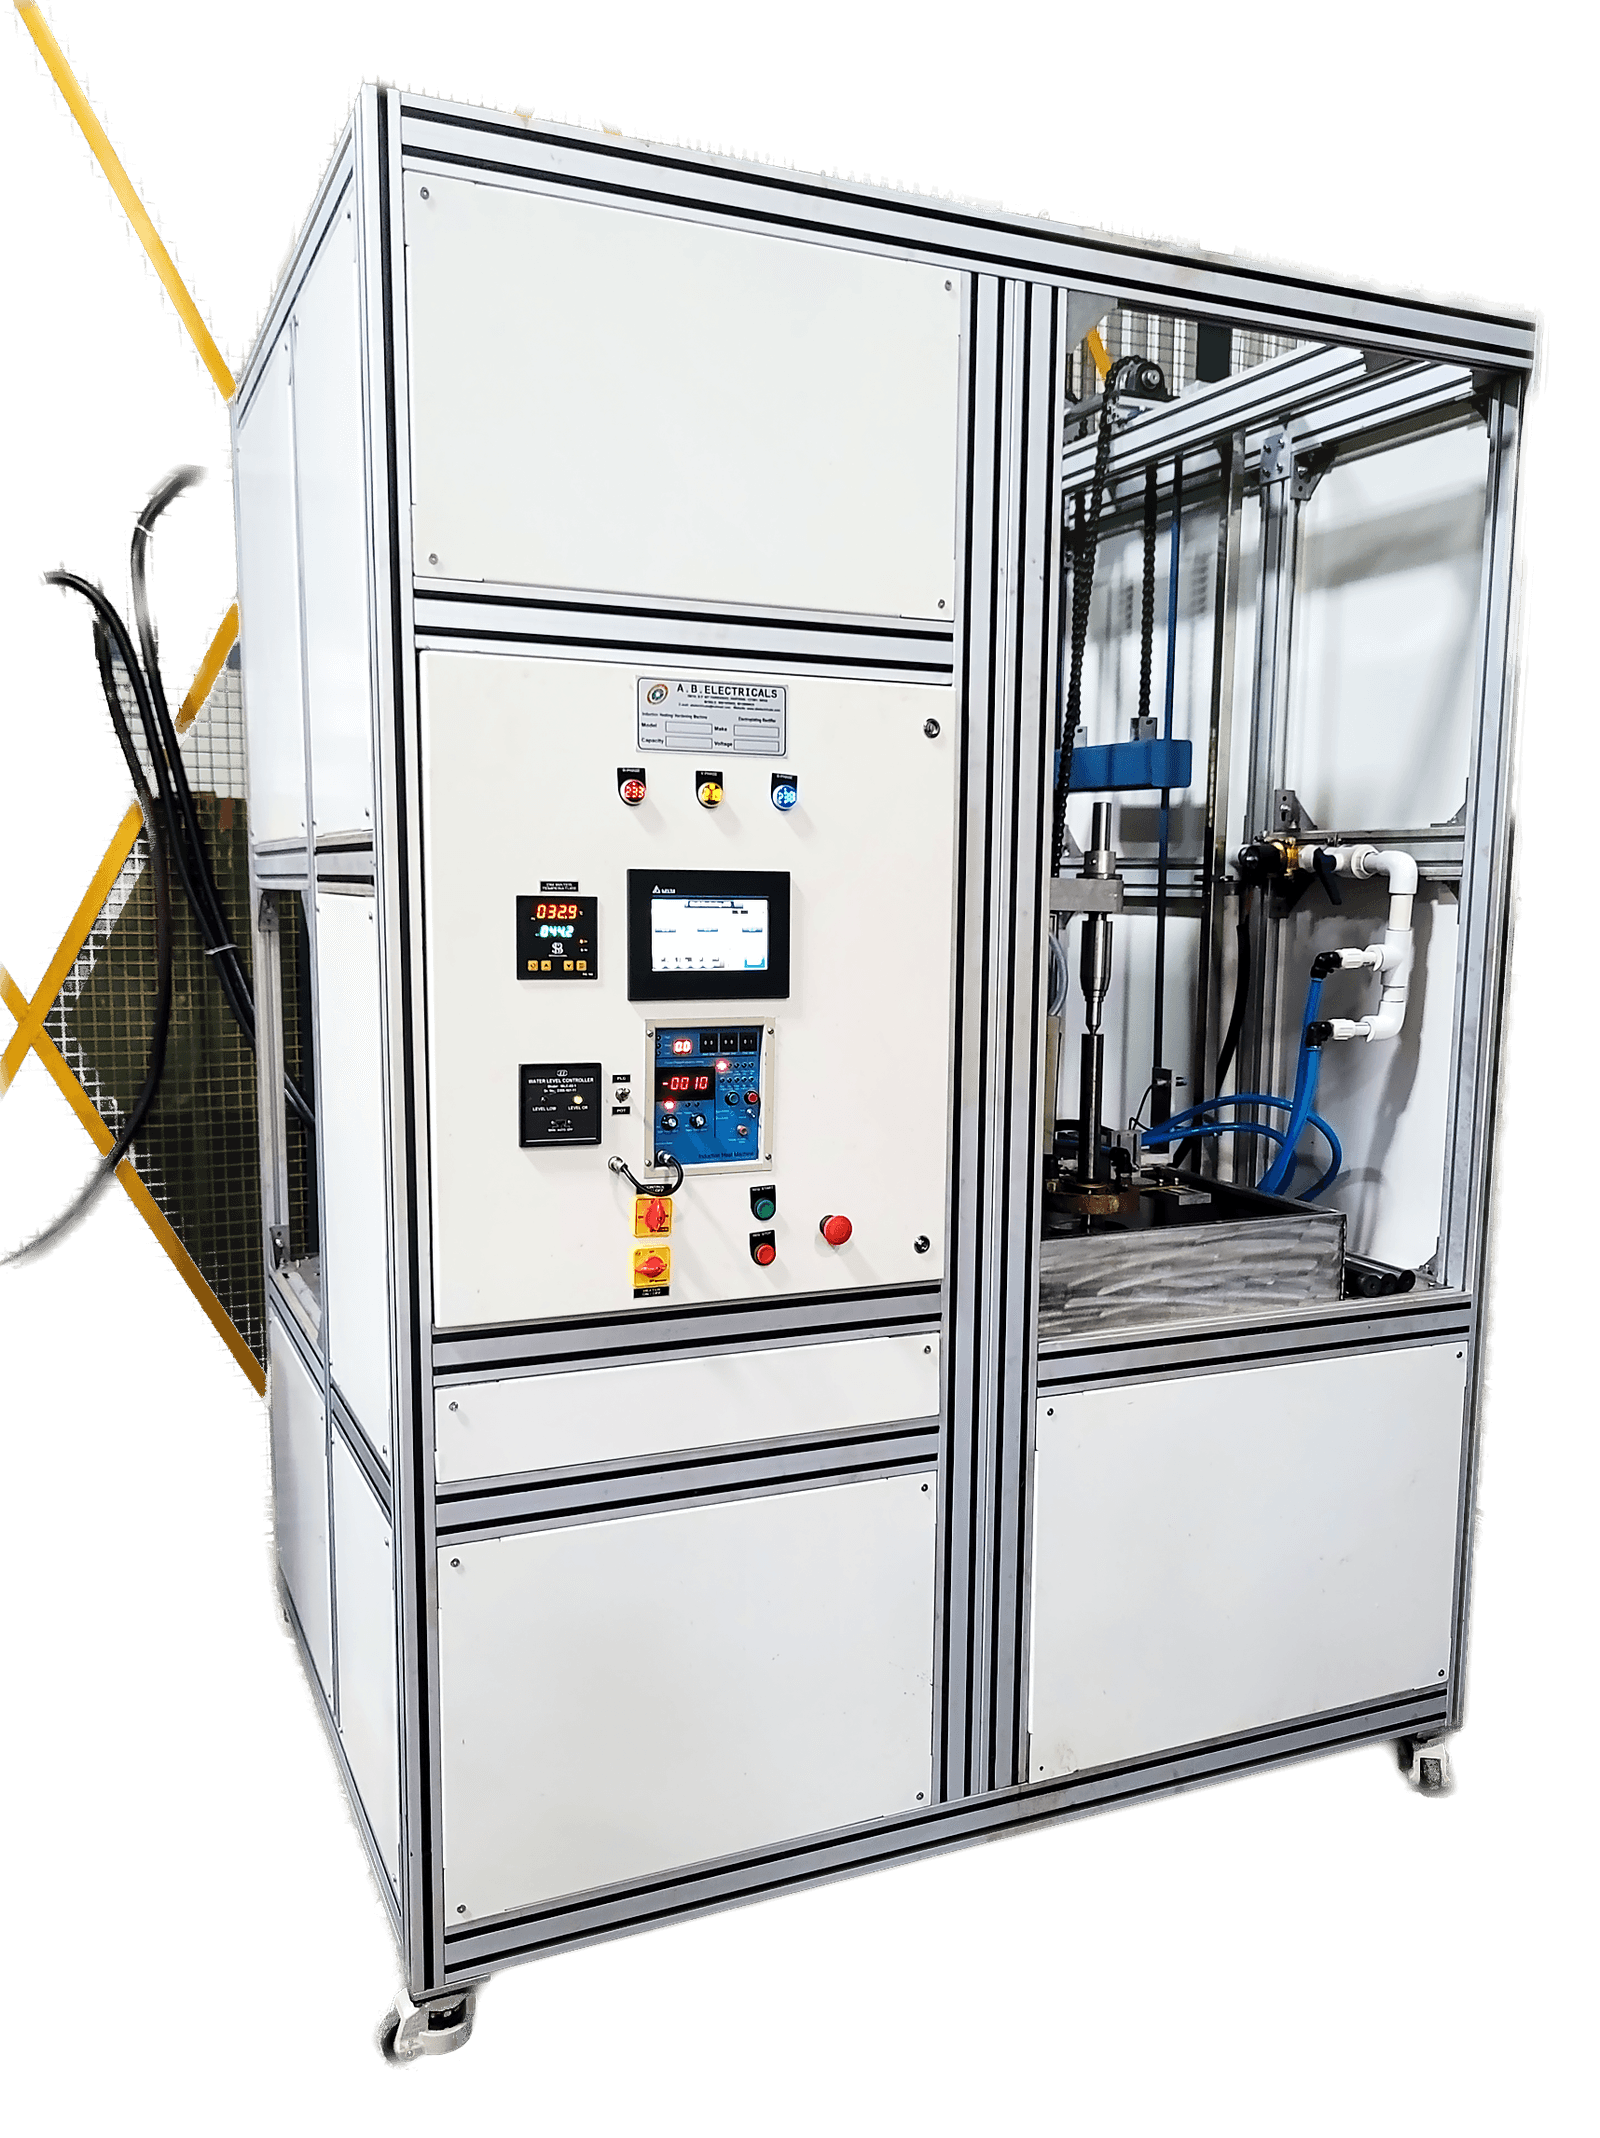
Axle shaft hardening on a vertical scanner
Hardening a shaft longer than any coil could heat at once.
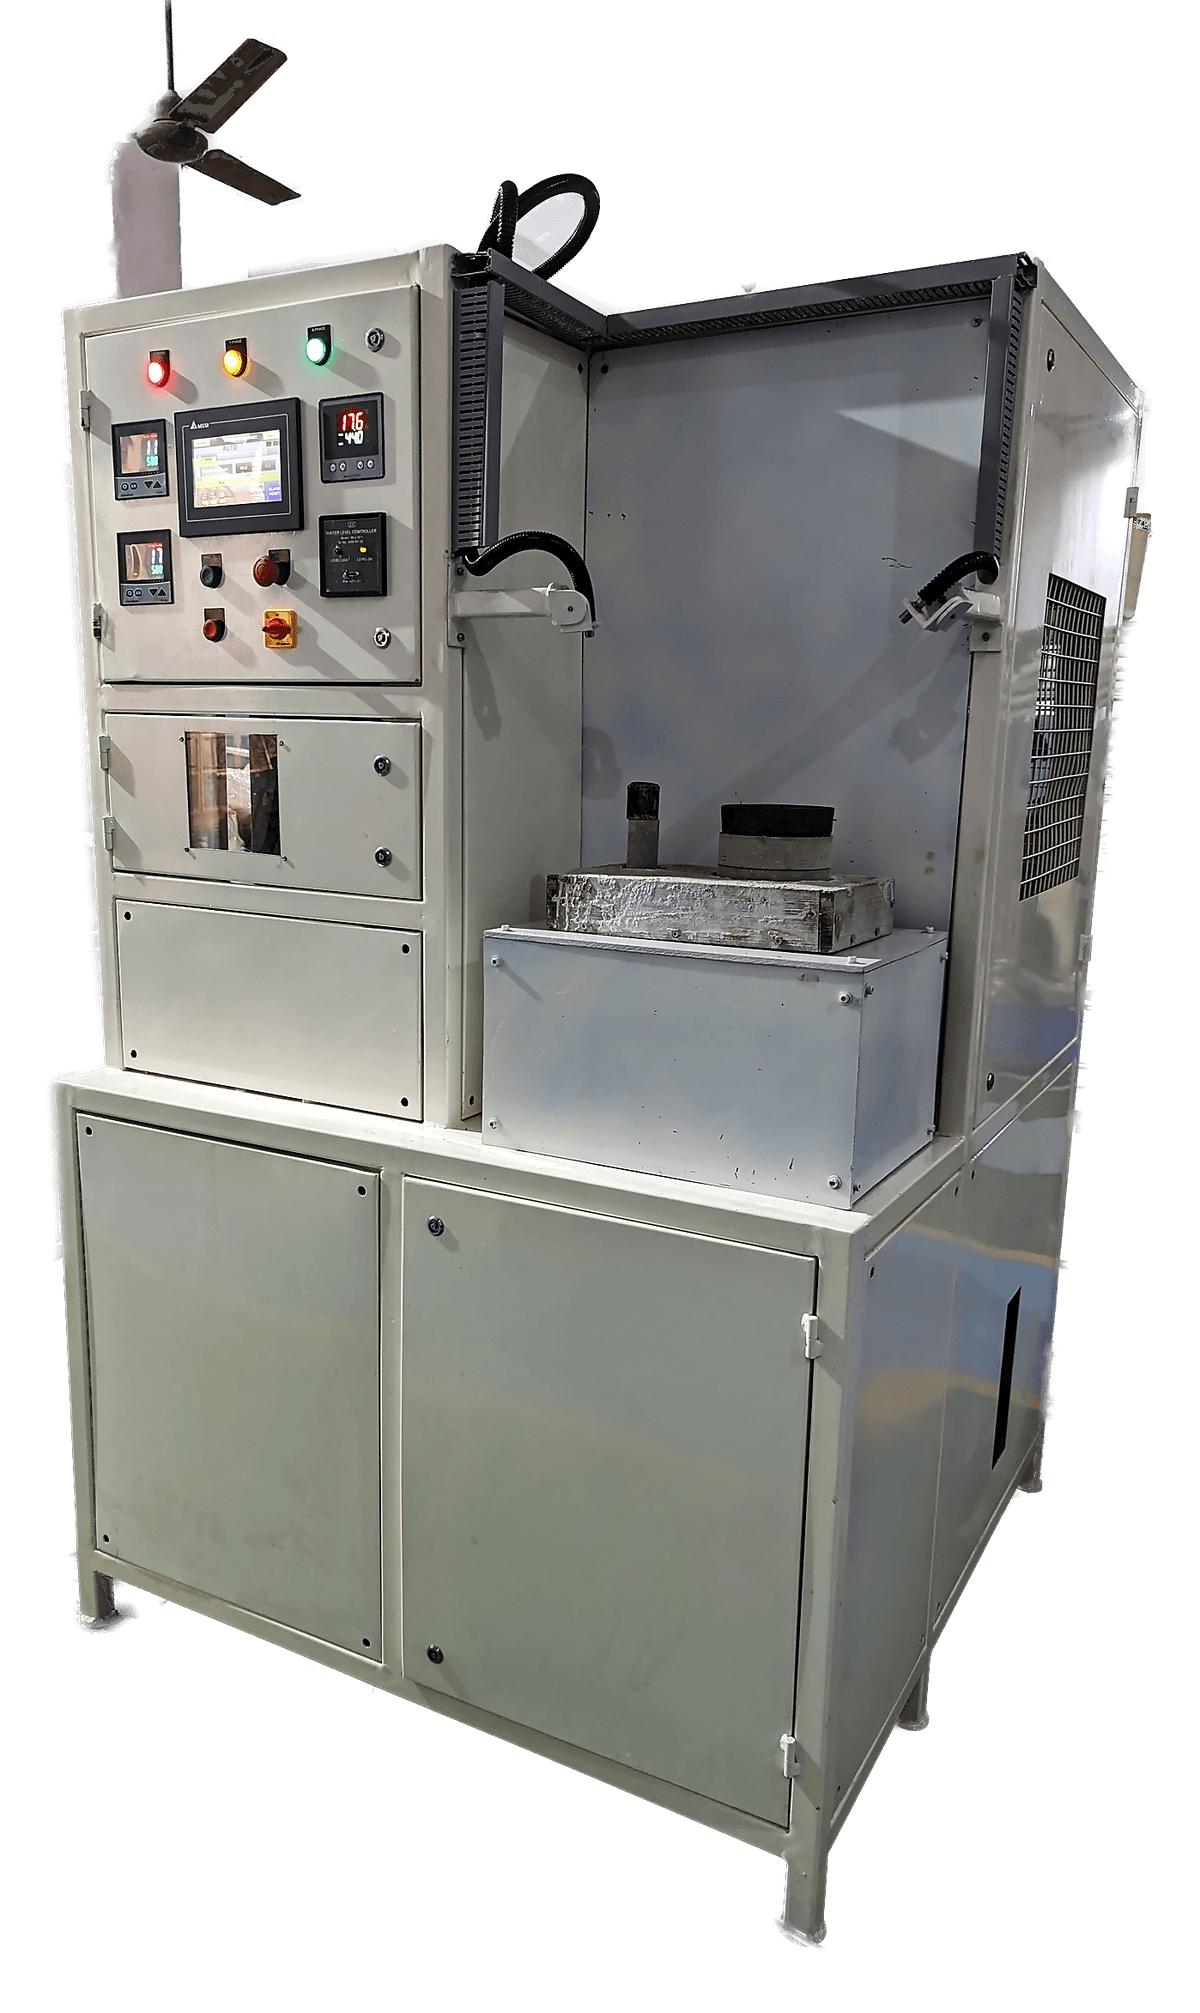
CI ring and bush heated together, in one operation
Two components, two correct temperatures, one cycle.
Let us look at your component.
Send us your drawing and tell us what the part needs to do. We will work through the process and machine requirements with you.