
CI ring and bush heating machines
Fully automatic PLC machines that pre-heat cast iron rings and bushes under closed-loop temperature control.
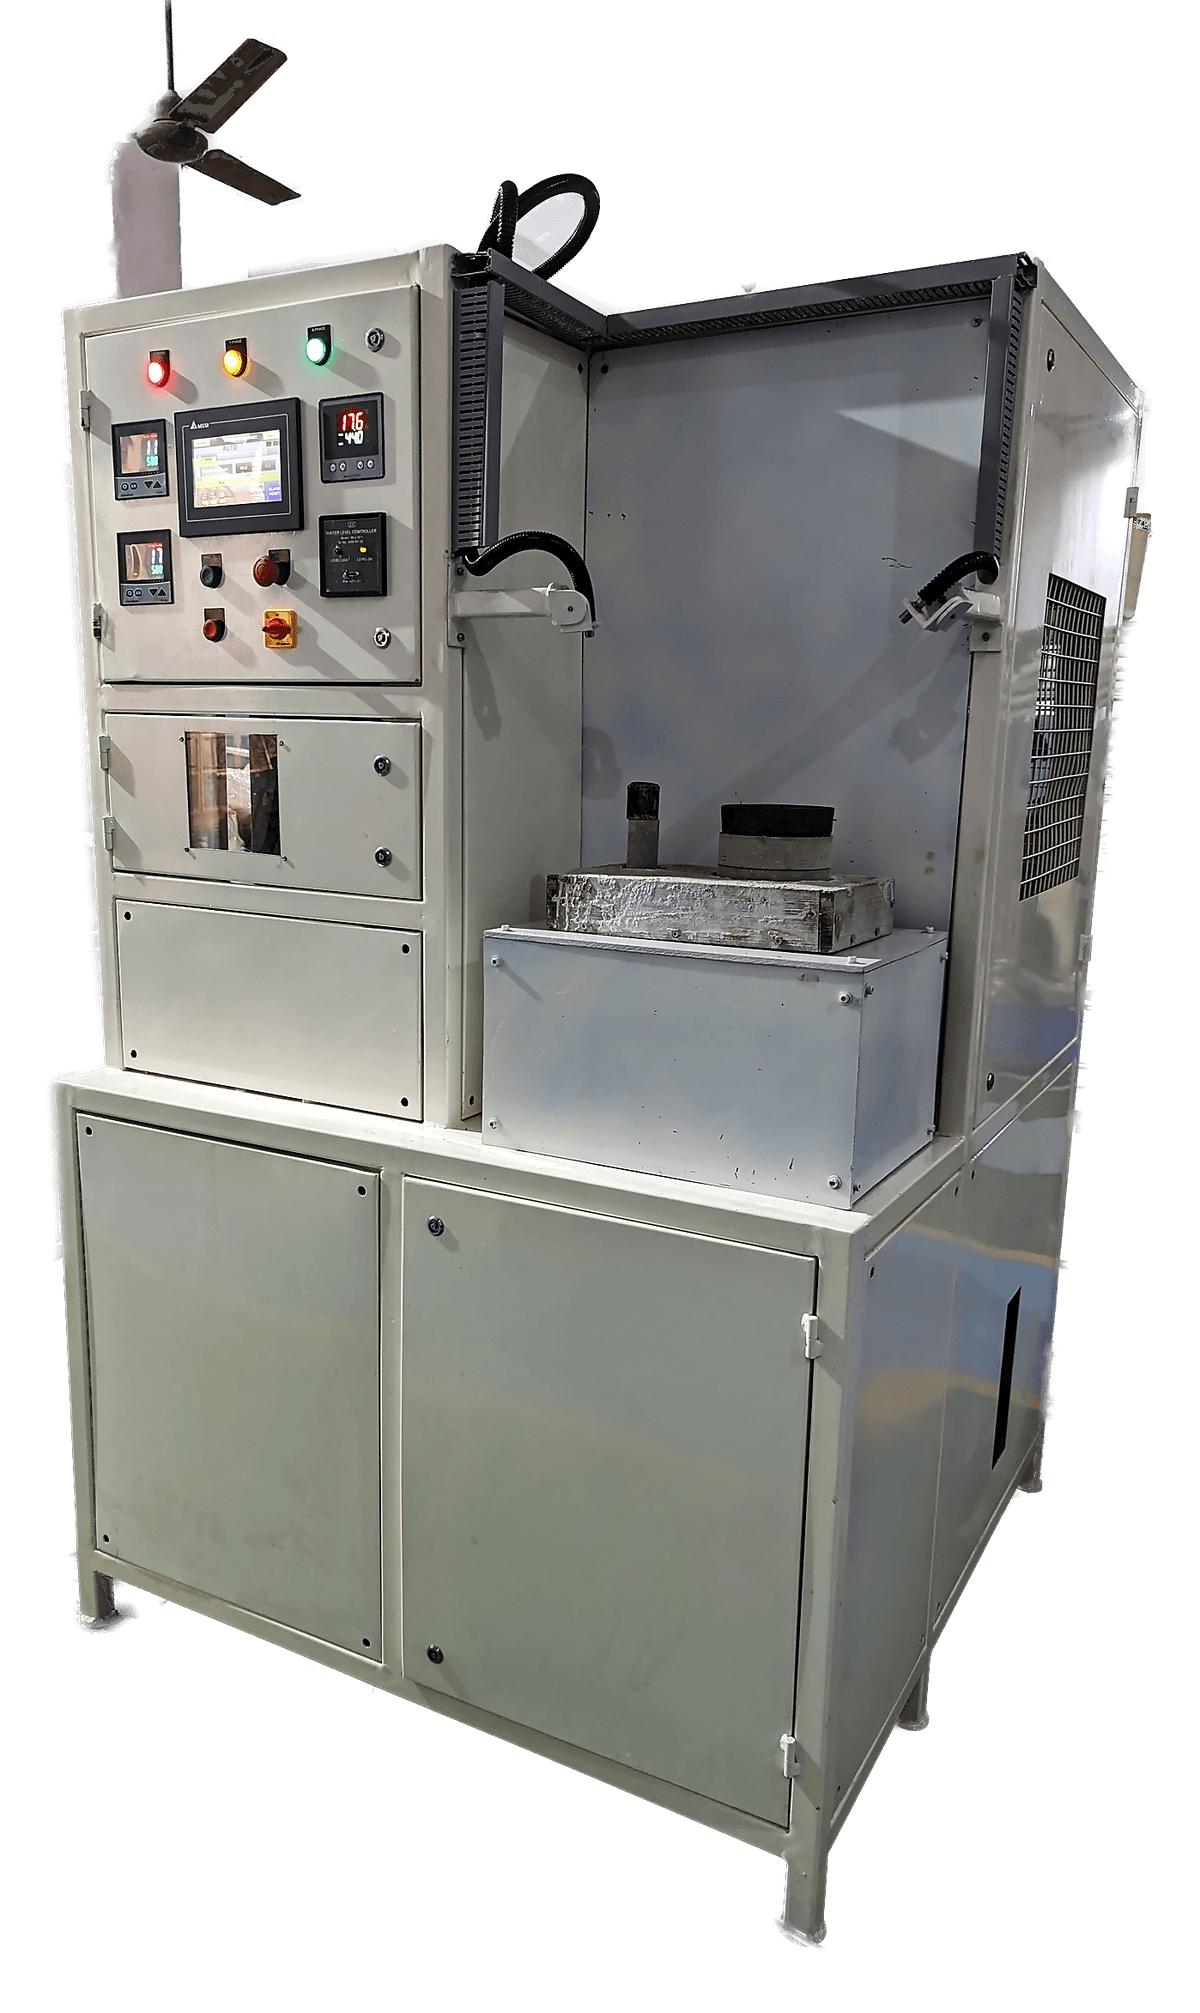
The alloy wheel industry pre-heats cast iron rings and bushes before assembly. The temperature has to be right: too cold and the fit is wrong, too hot and the component is damaged or the cycle wastes energy and time. Doing it in an oven means waiting, and means every part in the batch shares one setting.
We build medium frequency machines designed specifically for this. The ABE-50AB CI ring and bush dual heating machine heats one bush and one CI ring together in a single operation with precise temperature control. The ABE-40AB CI ring heating machine handles rings alone.
The fully automatic version is a PLC controlled vertical heating station with an inbuilt DM water cooling system, working on a temperature-based heating cycle rather than a fixed time, so each part is taken to the set temperature regardless of its starting condition.
Technical specifications
- Power classABE-40AB and ABE-50AB, 40 kW and 50 kW
- FrequencyMedium frequency
- ControlPLC controlled, temperature based
- Dual heatingOne bush and one CI ring together in a single operation
- CoolingInbuilt DM water cooling system
We confirm the final configuration against your component, material and production requirements.
Questions engineers ask
Why temperature control rather than a timer?
Because parts do not all start at the same temperature. A part that has been sitting in the sun and a part straight off a cold rack need different amounts of energy to reach the same finish temperature. Closed-loop control on measured temperature gets both right; a fixed timer gets one right.
Why medium frequency for this?
Pre-heating wants the heat through the section, not concentrated at the surface. Lower frequency penetrates deeper, so the ring comes up to temperature more uniformly rather than getting a hot skin and a cold core.
Related processes
Tell us about the part.
Send a drawing, the material, the case depth or temperature you need, and your production rate. Our engineers will help define the right machine for your process.