
Induction power supply
ABE-120AB
120kW
Our 120 kW power supply for shaft hardening up to 120 mm diameter and flywheel ring hardening.
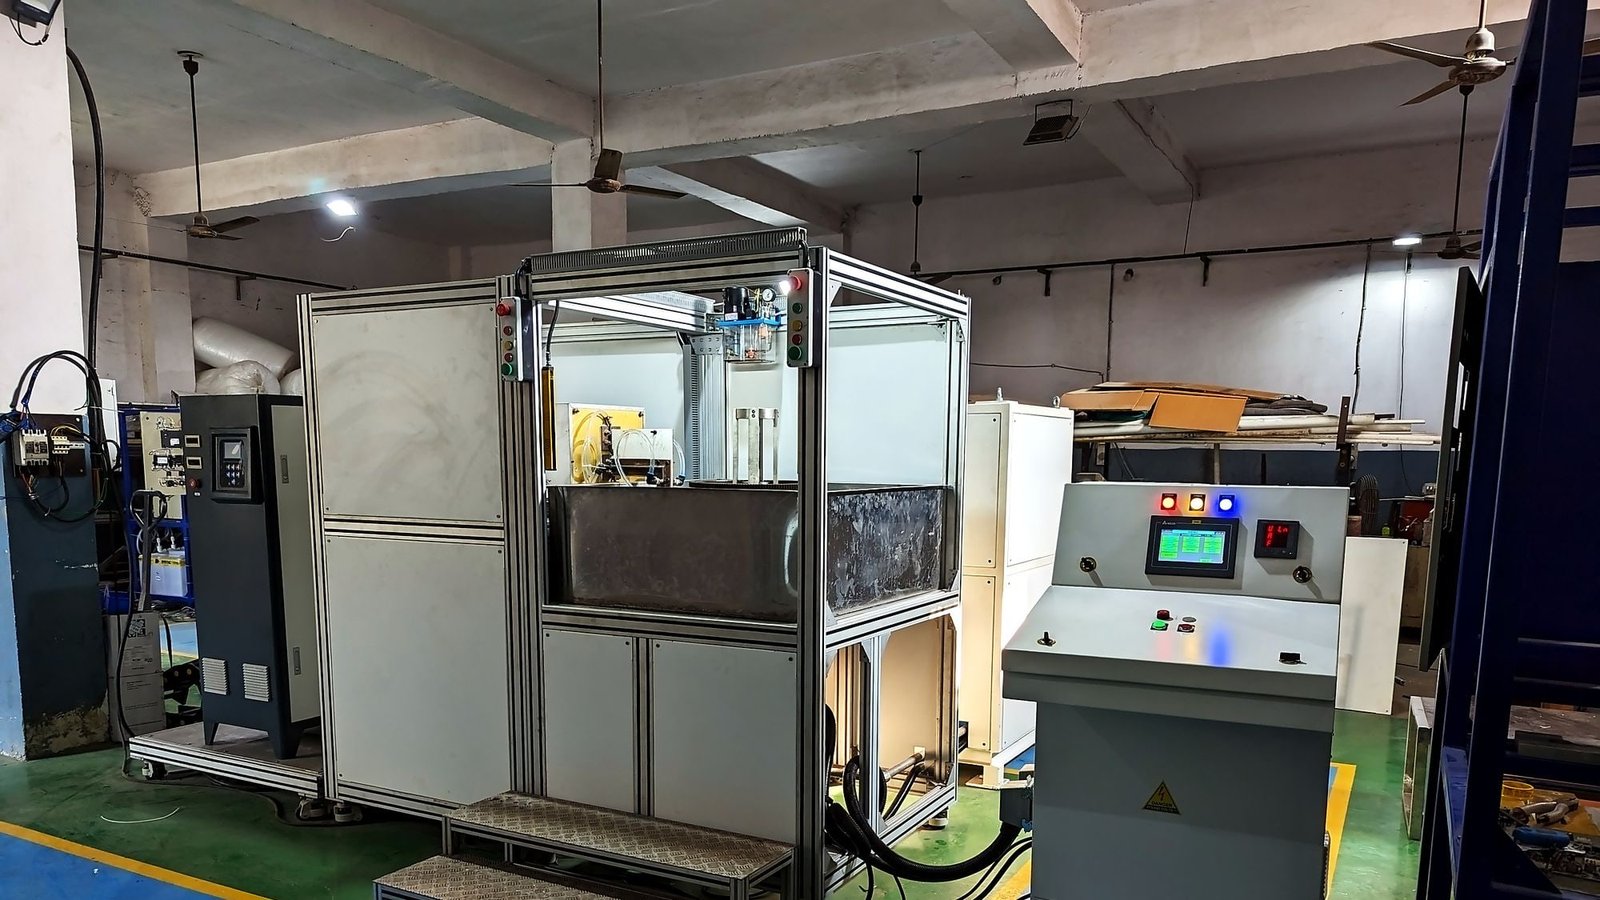
Our ABE-120AB provides 120 kW for end heating, hardening, tempering and billet heating in hand tool and auto component production.
Its best known application is flywheel ring hardening, where a starter ring gear is heated and hardened around its full circumference. We can customise the machine for shaft hardening up to 120 mm diameter, along with gears, bushes, JCB parts, tractor parts and axle shafts.
At the top of the vertical scanner rating, 120 kW is also the largest supply the PLC controlled scanner is specified to work with, covering shafts to 120 mm diameter, case depths from 0.8 mm to 5 mm and travelling lengths from 10 mm to 1500 mm.
Technical specifications
| Parameter | Specification |
|---|---|
| Output power | 120 kW. We confirm the duty cycle for your application. |
| Oscillation frequency | We select the frequency for your material, heating zone and required case depth. |
| Input power supply | We confirm the voltage, phase, frequency and connected load in your quotation. |
| Cooling water requirement | We specify the water flow, pressure, quality and cooling circuit for your machine configuration. |
| PLC / automation interface | Manual, PLC or CNC control options. We confirm communications and I/O with your automation requirements. |
| Compatible steels and alloys | We assess your material grade and heat treatment requirements before confirming suitability. |
| Maximum shaft diameter, hardening | 120 mm (4.72 in), subject to component and process review. |
| Switching technology | Solid-state IGBT |
Calculating required power? Run your cycle time on the Induction Power Estimator.
We select the frequency, dimensions, cooling and handling for your application. Send us your component drawing and required cycle time so we can confirm the complete machine specification.
Related processes
- Induction hardeningA hard, wear-resistant case on a tough core, in seconds, with the heat placed exactly where you want it.
- Induction temperingTrading a little hardness for a lot of toughness, in line with the hardening machine.
- Induction shrink fittingAssembling interference fits by expanding the outer part instead of forcing it on.
- Induction billet heatingSteel at forging temperature in seconds, paced to the press, with far less scale.
- Bar and end heatingHeating only the end of the bar that is about to be formed, and nothing else.
Related products
- Induction heating machinesIGBT power supplies from 5 kW to 500 kW, supplied standalone or built into a PLC or CNC controlled machine.
- Induction hardening machinesVertical and horizontal hardening machines for shafts, gears, bushes, axle shafts and flywheel rings.
- PLC controlled vertical hardening scannersA scanning hardening machine: the part traverses through the coil while quench follows behind it.
- Billet and bar heating systemsBillet heaters from 50 kW to 300 kW, and bar end heaters for forging lines.
- Flywheel ring hardening and shrink fitting machinesTwo processes on one component: hardening the starter ring gear, and shrink fitting it onto the flywheel.
Tell us about the part.
Send a drawing, the material, the case depth or temperature you need, and your production rate. Our engineers will help define the right machine for your process.