
Induction heating machines, designed and built in India
IGBT power supplies from 5 kW to 500 kW, supplied standalone or built into a PLC or CNC controlled machine.
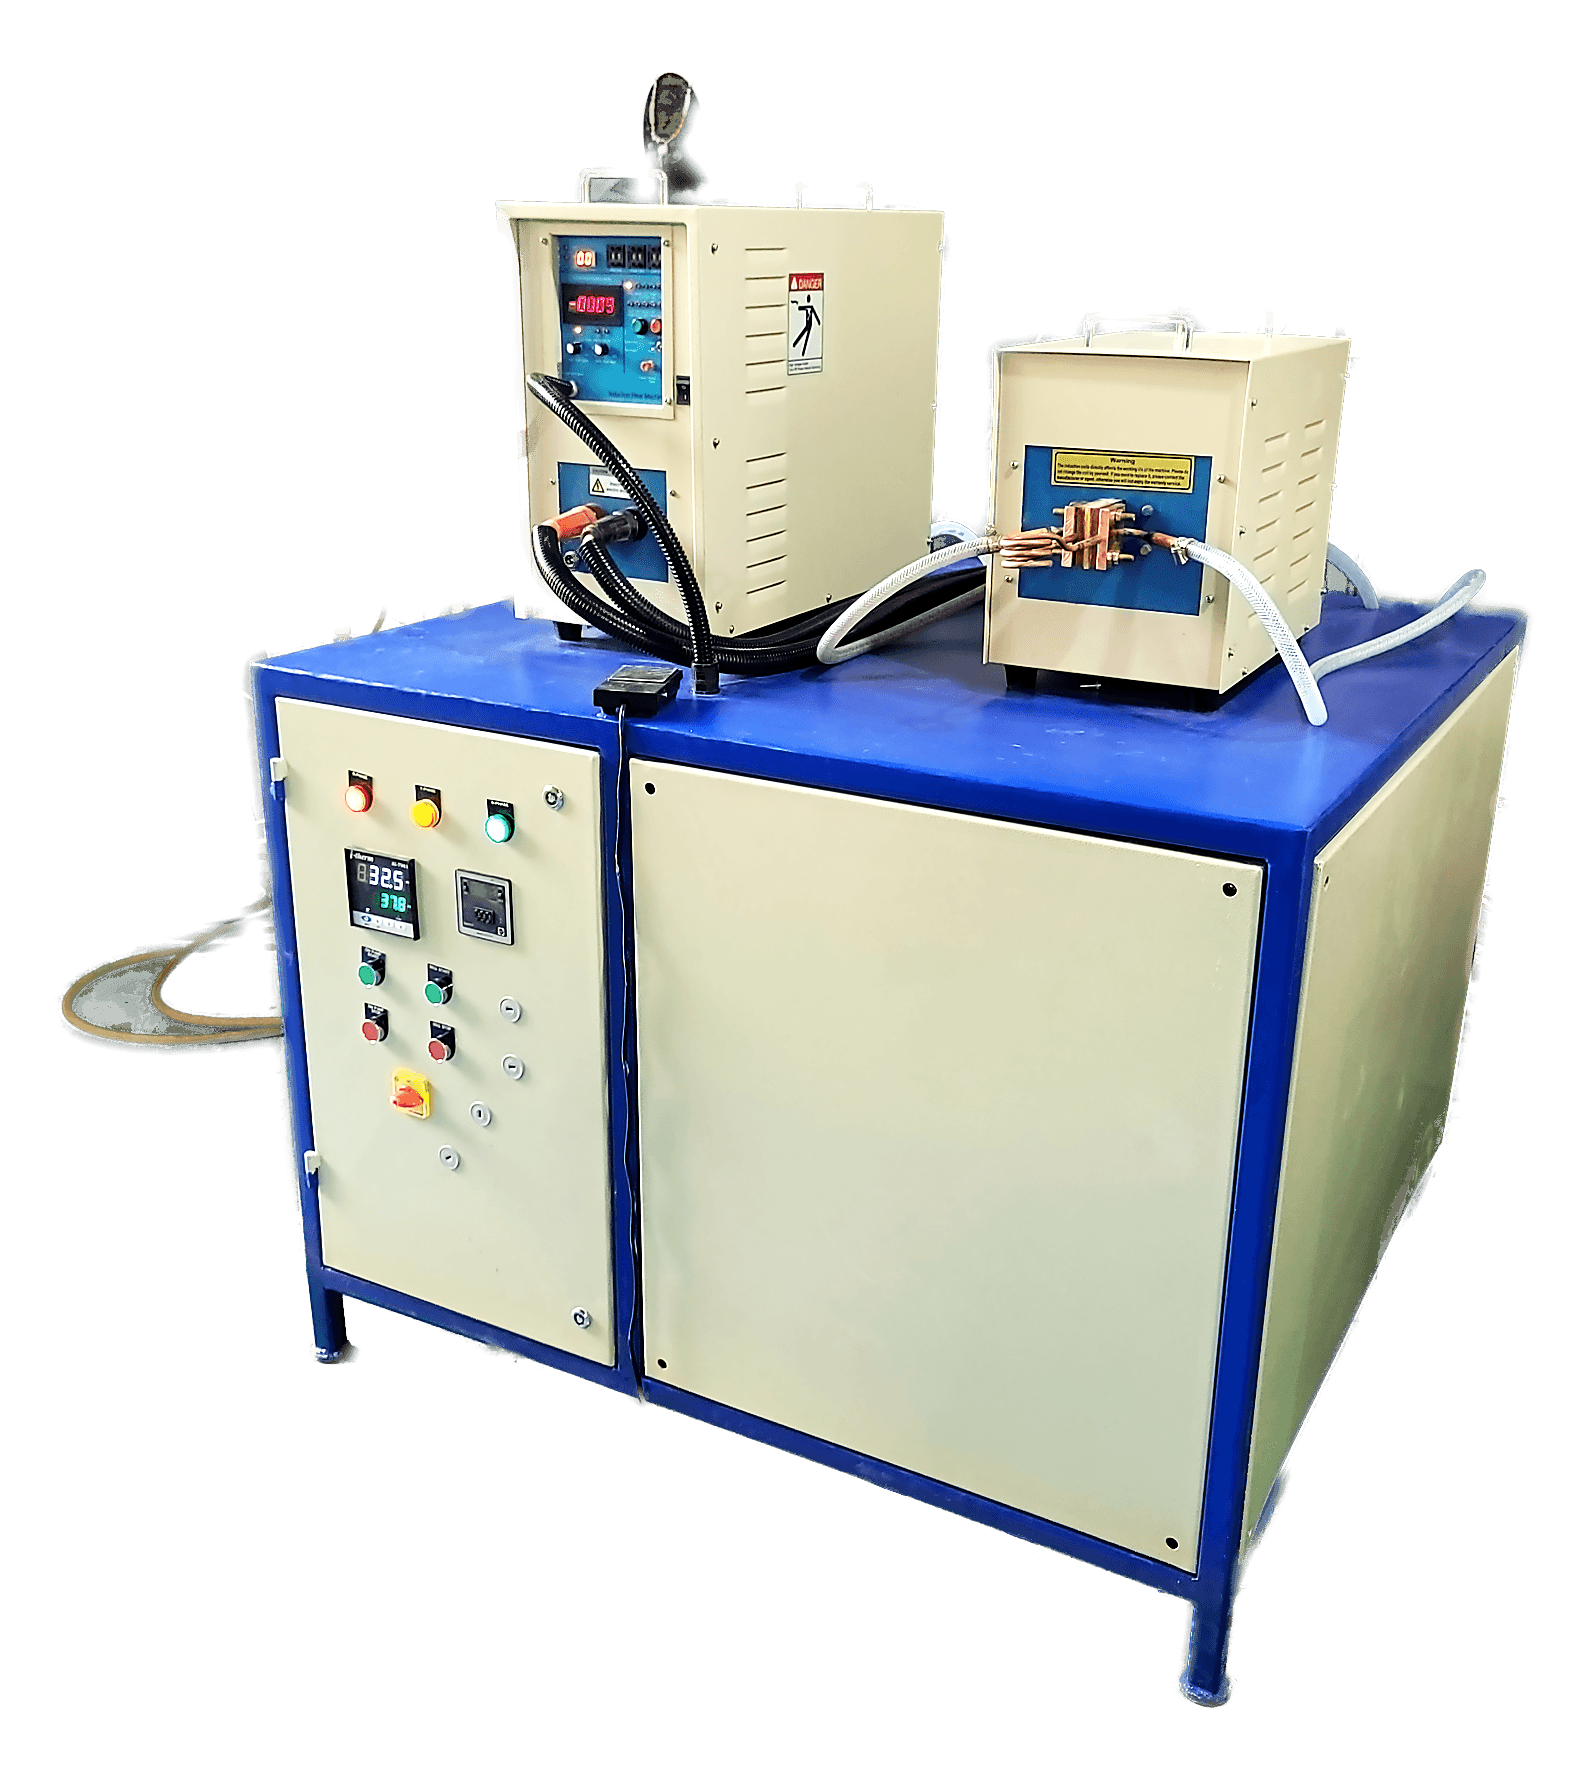
We use induction to heat the workpiece directly. An alternating current in a copper coil creates a magnetic field that induces currents in the part. Electrical resistance converts those currents into heat, allowing us to concentrate heating in the area your process requires.
A.B. Enterprises (AB Induction) has designed and built these machines at our works in N.I.T. Faridabad, Haryana, since 2001, for forging, auto component, tractor, hand tool and motor manufacturers. Our range runs from 5 kW to 500 kW across medium, high and ultra high frequency, and the frequency is selected for the application rather than the other way round.
Medium frequency machines are specified for billet heating, end heating for forging, hand tool and auto component work, and shrink fitting of bearings, gears and motor housings. High frequency machines are specified for induction hardening of auto components, tractor parts, hand tools and agricultural tools, and for brazing. Ultra high frequency machines suit fine brazing work, small joints and thin sections. Our guide to frequency, power and case depth explains how the band is chosen.
Every machine can be supplied as a bare power supply, or as a complete system with the coil, the cooling, the handling and the control designed around your part.
Technical specifications
- Power range5 kW to 500 kW
- Switching technologyIGBT
- FrequencyMedium, high and ultra high frequency, selected per application
- ControlManual, PLC or CNC
- CoolingDM water cooling and circulation; DM water chiller where duty requires it
We confirm the final configuration against your component, material and production requirements.
Induction heating machines we build
Alongside the ABE power supplies above, we build complete induction heating machines for specific processes, each configured around your component.
Machines by process
- Billet and bar heating systemsBillet heaters from 50 kW to 300 kW, and bar end heaters for forging lines.
- Induction hardening machinesVertical and horizontal hardening machines for shafts, gears, bushes, axle shafts and flywheel rings.
- Induction brazing machinesRepeatable brazed joints with heat placed only where the filler must flow. Single and double station.
- Induction bonding machinesPLC controlled rotary machines for heat-activated bonding under controlled temperature and time.
Application-specific machines
- CI ring and bush heating machinesFully automatic PLC machines that pre-heat cast iron rings and bushes under closed-loop temperature control.
- Flywheel ring hardening and shrink fitting machinesTwo processes on one component: hardening the starter ring gear, and shrink fitting it onto the flywheel.
- Drum heating machinesHeat put into the drum wall itself, for viscosity reduction and temperature maintenance without a flame.
Machines we have built
- CI ring and bush heated together, in one operationTwo components, two correct temperatures, one cycle.
- Flywheel starter ring hardening at 120 kWHardening a starter ring gear all the way round, at consistent depth.
- Compare the ABE rangePower, shaft diameter and the processes each ABE model is specified for.
- Induction power estimatorA first-pass power figure from the mass you heat, the temperature rise and the rate.
Questions engineers and buyers ask
What power rating do I need?
Power is set by how much mass you must heat, how far you must raise its temperature, and how quickly. A small brazed joint may need 15 kW; a forging billet line may need several hundred. The power estimator on this site will give you a first-pass figure from those three inputs, and the real number comes from looking at your part.
What does IGBT mean in practice?
IGBT is the semiconductor switch used in the inverter. Compared with older thyristor and valve designs it switches faster and more efficiently, which means a smaller, lighter, cooler-running machine that wastes less of your supply as heat.
Can the machine be automated?
Yes. We build PLC and CNC controlled automatic machines around the same power supplies, sized to your application and production requirement.
Where are your induction heating machines made?
At our own works at Plot No. 89, Bhakri Industrial Area, N.I.T. Faridabad, Haryana, where A.B. Enterprises has designed and built induction machines since 2001. Our design, production, quality control, research and development, and testing teams work together there. You are welcome to arrange a visit.
Which frequency do I need?
We build medium, high and ultra high frequency machines and select the band for the job. Medium frequency penetrates deeper and suits billet heating, bar end heating, shrink fitting and pre-heating. High frequency suits hardening of auto components, tractor parts and hand tools, and brazing. Ultra high frequency suits fine brazing work, small joints and thin sections. See frequency, power and case depth.
What do you need from me to quote?
Send us your part drawing, material grade, treated zone, required case depth or temperature, and production rate. Tell us what happens before and after heating so we can plan the handling and controls. If some details are still open, we can work through them with you. The quote form asks for these details.
Do you supply machines outside India?
Yes. Contact us with your destination, electrical supply and project requirements. We will discuss a suitable machine and the delivery arrangements for your location.
Related processes
- Induction hardeningA hard, wear-resistant case on a tough core, in seconds, with the heat placed exactly where you want it.
- Induction brazingJoints that come out the same every time, because the heat is placed by a coil and timed by a machine.
- Induction billet heatingSteel at forging temperature in seconds, paced to the press, with far less scale.
- Bar and end heatingHeating only the end of the bar that is about to be formed, and nothing else.
- Induction shrink fittingAssembling interference fits by expanding the outer part instead of forcing it on.
- Induction pre-heatingBringing a component to a controlled temperature before the operation that follows.
- Induction annealingSoftening metal, relieving stress and restoring formability, on the section that needs it.
Industries served
- ForgingSteel at temperature at the rate the press works, with far less scale than a furnace.
- Automotive componentsShafts, gears, bushes, axle shafts and flywheel rings, at production rate.
- Hand toolsSledge hammers, claw hammers, chisels, pick axes and hoes, forged and hardened.
- Tractor and agricultural equipmentParts that work in soil and abrasion, where wear resistance decides service life.
- Motors and electrical manufacturingHousings, stators, bearings and gears, assembled by expansion rather than force.
- Alloy wheels and castingsCI ring, drum and bush pre-heating, under closed-loop temperature control.
How buying a machine works
- Send us the part. Your drawing, material grade, the zone to be treated, the case depth or temperature you need, and your production rate. If some details are still open, we can work through them with you.
- We review your component. Our team will look at your requirements and ask for any details we need to assess the application.
- We discuss the process. We will work through the power, frequency, coil, handling, cooling and controls with you.
- We prepare your proposal. We set out the machine configuration and scope. Ask us to confirm installation and commissioning, operator training, warranty and recommended spares in your proposal.
Send a quick enquiry
Tell us about the part and the heating job. Our engineers will come back to you to define the right machine.
Tell us about the part.
Send a drawing, the material, the case depth or temperature you need, and your production rate. Our engineers will help define the right machine for your process.